Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

News

Enerpac launches Armor Stack modular tool storage and deployment system

Industrial hydraulic tools specialist, Enerpac, announces Armor Stack, the first heavy-duty tool storage platform that combines military-rated protection in a fully modular, stackable system. Developed by Enerpac, it delivers the rugged durability needed to protect valuable hydraulic tools while giving users the flexibility to organise, transport, and deploy tools more efficiently.
Until now, companies deploying maintenance and construction teams across multiple sites have faced significant logistics and practical challenges. Traditional heavy-duty toolboxes operate as standalone units; Armor Stack changes the model, allowing multiple cases to lock, stack and deploy as a single integrated system. This enables teams to create scalable, job-specific tool configurations required for each application. The result is faster deployment, better organisation and greater flexibility in the field, while securely keeping critical hydraulic tools together and ready for use in the toolbox’s pre-cut foam interiors.
Armor Stack C8 Leads the Enerpac Launch
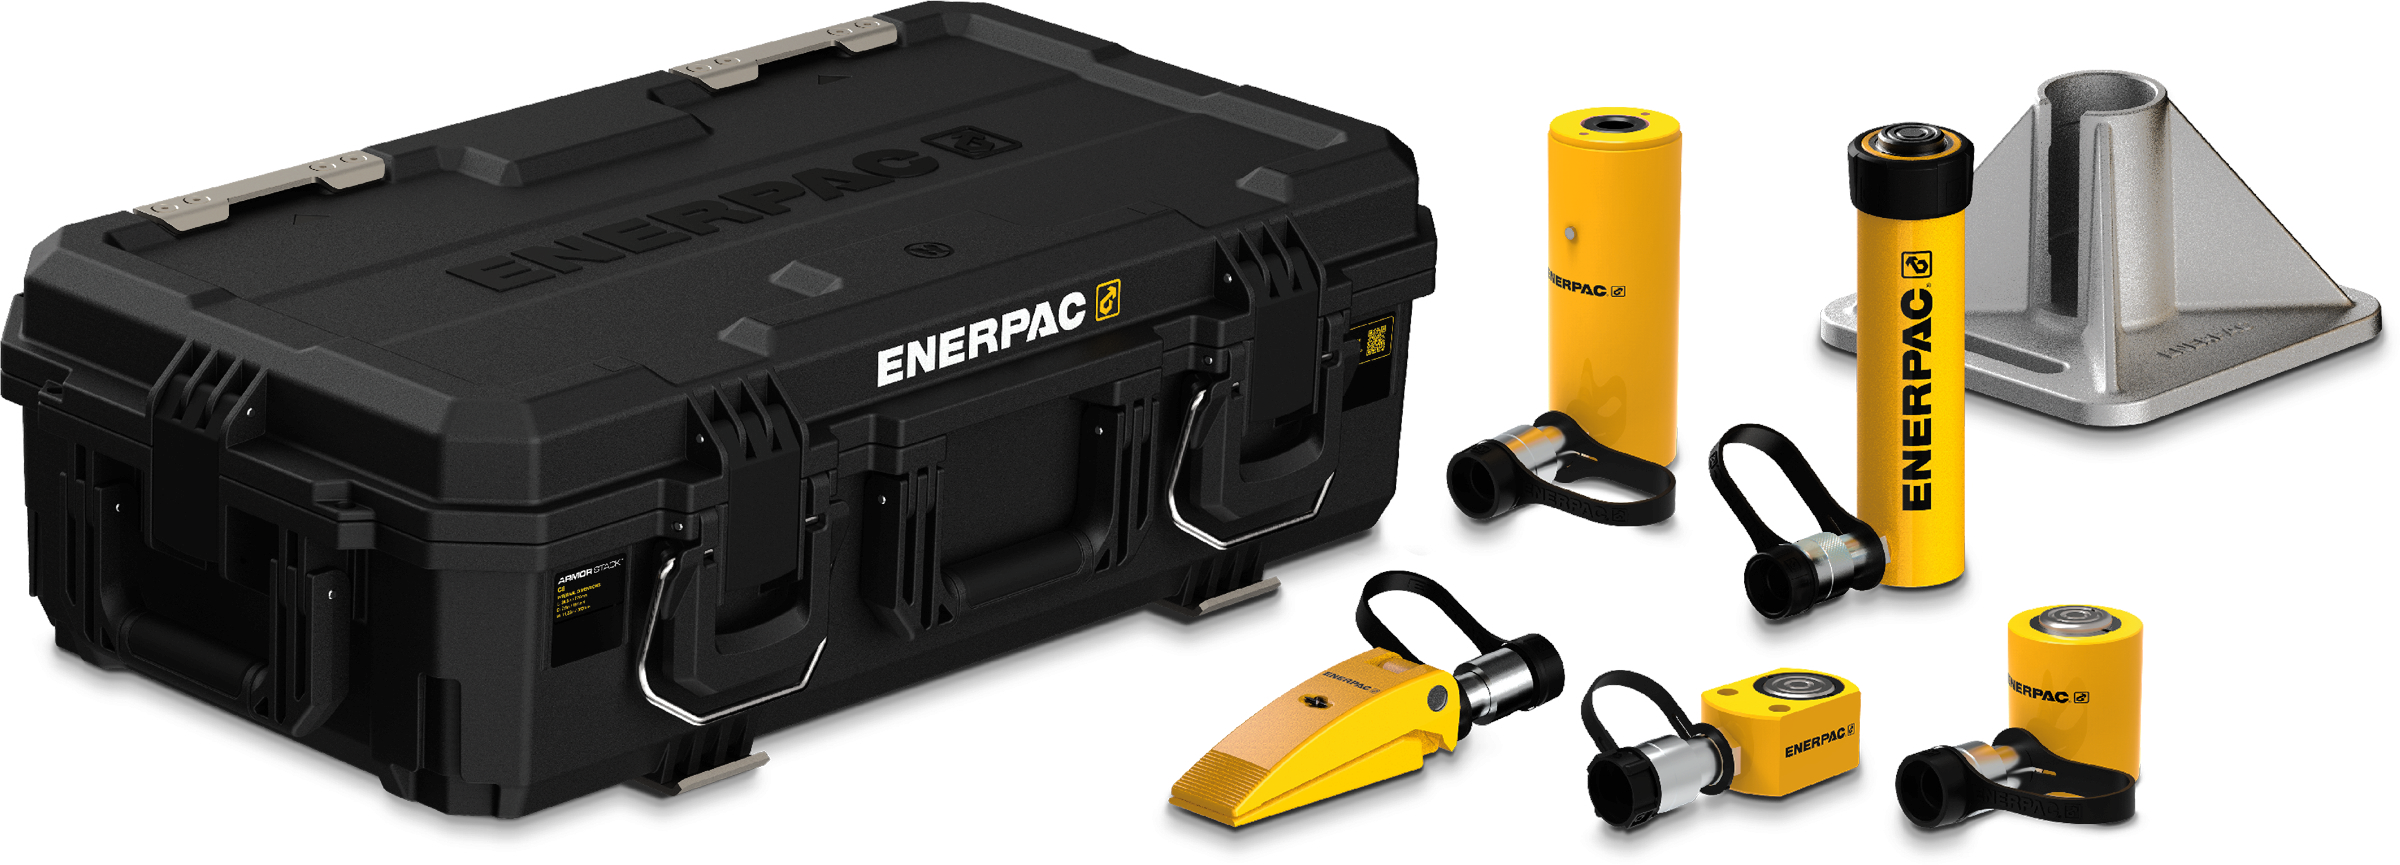
Enerpac launches Armor Stack with the medium-sized C8 configuration, providing customers with the full benefits of the modular, stackable system from day one. The Armor Stack ARMRC8 range of cases is available in five configurations: three hand pump kits, a 101 kN tonne hydraulic lifting kit, and a 101 kN hydraulic lifting kit with hand pump. In addition, an empty Armor Stack stackable case is available for storing existing tools.
For easier handling, the Armor Stack toolbox features over-moulded heavy-duty handles designed to provide a secure grip when lifting and moving equipment, helping teams transport their tools safely across workshops, plants and job sites. A separate wheel kit comprising two attachable wheels allows larger, heavier cases to be moved around easily. For stacked toolboxes, the Armor Stack range also includes a custom Enerpac trolley for ease of site deployment.
Further sizes and configurations are planned for future release, expanding the platform to meet a wider range of tool storage, transport and deployment requirements.
"Traditional heavy-duty toolboxes generally operate as standalone units, which limits flexibility on complex job sites," says David Proeber, Director, Strategic Growth + Innovation at Enerpac. "Armor Stack changes the paradigm entirely by bringing military-grade protection to a fully integrated, modular system. Every contour, latch, and handle was designed specifically around the real-world demands of field technicians and maintenance teams, delivering protection for high-value hydraulic assets and significantly streamlining site planning and logistics."
Modular, stackable tool storage system designed around the job
Armor Stack heavy-duty, industrial toolboxes are engineered to withstand the rigours of real-world industrial use. Every Armor Stack case is validated against Military Standards MIL-STD-810-H, ensuring the C8 cases are resistant to harsh environmental stresses like drops, extreme temperatures, and vibrations. They are also ATA 300 specified and IP67 validated, protecting high-value, sensitive tools against dust and water immersion.
Armor Stack utilises an integrated metal latching system that allows multiple cases to be securely locked, stacked, and transported as a single tower unit weighing up to 226 kg. Reinforced, padlockable security points provide additional protection during storage and transit, while wind-resistant hinged lids help keep cases securely open during use.
By combining robust protection with a modular, stackable design, Armor Stack provides a new approach to transporting and deploying tools, helping teams arrive on site with the tools they need, organised and ready to work.
For more information on the Enerpac Armor Stack system, visit www.enerpac.com
 

Dräger strengthens defence sector capability with key hire 

Screenshot 2026 10 12 145300

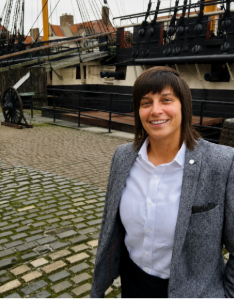
Dräger, an international leader in the fields of medical and safety technology, has appointed Jennie Danton as Defence and Security Business Development Manager to strengthen its support for defence customers and help highlight how its technologies, national resilience capabilities and sector expertise can support operational readiness across defence.

Jennie previously served in the Royal Military Police (RMP). Since leaving the military, she has built a decade of industry experience and held a range of defence-focused commercial roles spanning submarine gas detection and monitoring systems, shipbuilding, and unmanned aerial vehicle (UAV) technology.

She joins Dräger’s Government team with a strong understanding of customer requirements, operational challenges and the wider defence landscape.

In her new role at Dräger, Jennie will focus on developing and growing Dräger’s presence within the UK defence sector. She will be responsible for identifying new opportunities, building strong relationships and helping customers better understand how Dräger’s technologies and expertise can support them. She will help position Dräger as a business, well equipped to respond to current and emerging needs, support operational readiness and national resilience across defence.

Jennie says she is excited by the opportunity to combine commercial growth with a clear sense of purpose:

“What drew me to Dräger was its focus on protection and survivability. The opportunity to build and shape the defence business for Dräger in the UK, bring new ideas on board and strengthen the foundations already in place is incredibly exciting.

“With my military background, it means a great deal to be able to help people understand the technologies available to protect them in some of the most challenging environments – whether that’s military operations, firefighting or responding to chemical, biological, radiological, and nuclear (CBRN) threats. Knowing I can contribute to keeping people safe gives this role real purpose.”

Matt Evans, Head of Government for UK and Ireland Safety Division, who Jennie will report to, says Jennie is a valuable addition to the team:

“Jennie brings first-hand military experience and a strong commercial background across defence, safety and adjacent technologies. Her first-hand understanding of customer requirements, combined with her passion for protecting people in operational environments, will be a real asset as we continue to strengthen our support for defence customers and promote national resilience.”

www.draeger.com


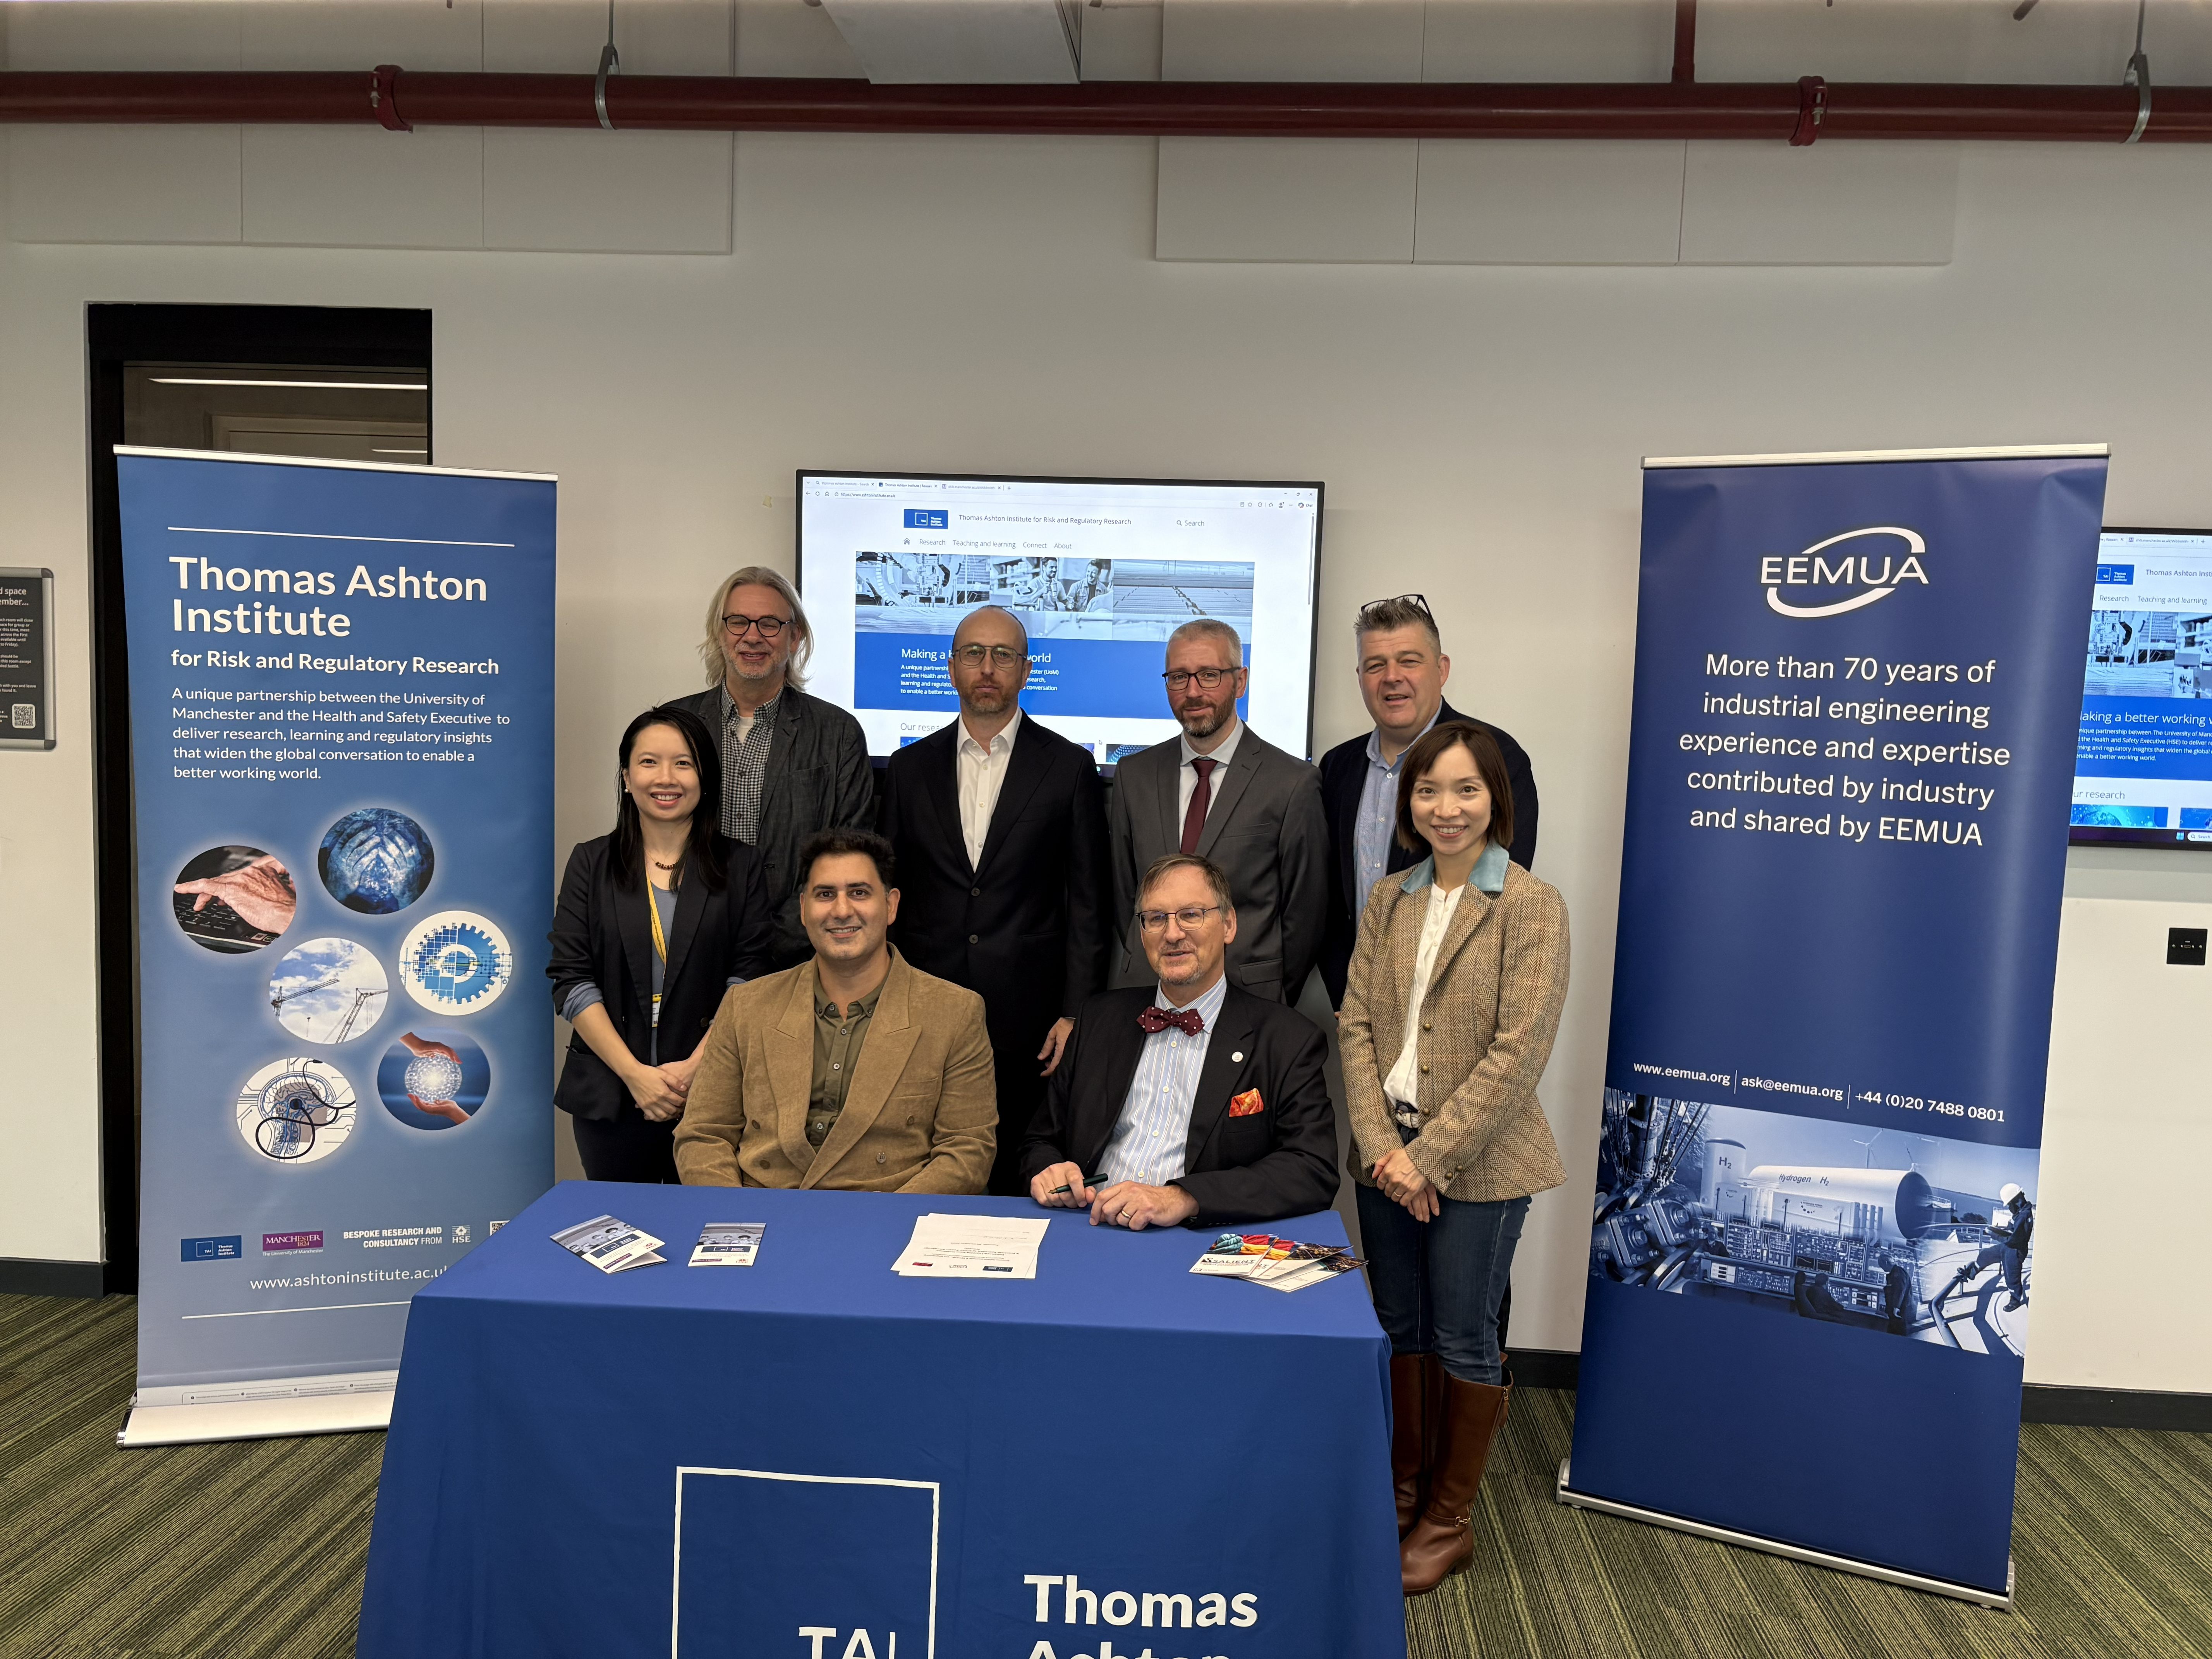
EEMUA, Thomas Ashton Institute, and University of Manchester launch joint research project to strengthen learning from industrial incidents

The Enhanced Learning from Incidents (ELFi) project aims to understand and provide both insight and potential solutions to ensure lessons learned in one sector of society or industry help prevent injuries and accidents in another.

Each year, millions of workers worldwide lose their lives due to occupational accidents and work-related diseases, while millions more experience non-fatal work-related injuries. Despite decades of safety improvements, similar incidents continue to occur across industries, often because vital lessons remain locked in silos, delayed by legal processes or buried in technical reports.

The Thomas Ashton Institute (TAI), the University of Manchester (UoM), and EEMUA (the Engineering Equipment and Materials Users Association) today announce the start of the Enhanced Learning from Incidents (ELFi) project, a research initiative developed with the Hazards Forum and other industry partners to change this.

Considerable work has already been done on incident investigation, root cause analysis and formal safety assessment to enable specific parties to learn from incidents. However, events with common causes still occur. Industry and regulators increasingly recognise that the challenge is not simply identifying lessons, but ensuring that organisations see their relevance, link them to their own sites and operations, act on them effectively and embed the learning sustainably. This is especially true when incidents occur outside an organisation's own sector, or even apparently unrelated activity.

Drawing on TAI's and UoM’s rigorous analysis and specialist expertise, the project will:

  • Analyse how incidents are reported, investigated, and shared across sectors
  • Identify barriers and enablers to effective learning and cross-sector knowledge transfer, including siloed or inconsistent reporting systems and cultural resistance to disclosure
  • Define best practice for incident reporting and sharing
  • Develop a practical cross-sector learning framework, toolkit, and adoption roadmap
  • Work with regulators, trade associations, industry bodies, and the Hazards Forum to support real-world adoption and a cultural shift towards proactive learning

The aim is to deliver practical guidance and pilot-tested tools that help industry learn faster and apply lessons more effectively, saving lives, protecting assets and reducing environmental harm.

"EEMUA is committed to standards that improve safety and help prevent accidents. Good practice on investigating incidents already exists, but the real challenge is helping operators recognise how a lesson from any industry applies to their own site, and then act on it. We look forward to working with TAI and inviting our members to engage with this project and help shape tools that work in practice."
Dr Stefan Kukula, Chief Executive, EEMUA

"Organisations rarely lack incident reports; what is often missing is a reliable way to recognise when a lesson from another sector applies to them, and to act on it before a similar event happens. By working alongside EEMUA, its members, regulators and safety professionals from the outset, we will build a strong evidence base and then co-design and pilot a framework and toolkit that turn incident data into contextualised, actionable learning across sectors."
Professor Martie van Tongeren, Deputy Director, Thomas Ashton Institute

"Most industries already investigate their incidents carefully, but those lessons rarely travel beyond the sector, or even the site, where they happened. Over the course of this initiative, we'll work with EEMUA members, regulators, and safety professionals to find out why, and co-design a framework and toolkit that are tested on real industry cases rather than on paper. We'd welcome organisations from any sector that want to help shape it."
Dr Saeed Reza Mohandes, Principal Investigator, University of Manchester

http://www.eemua.org/

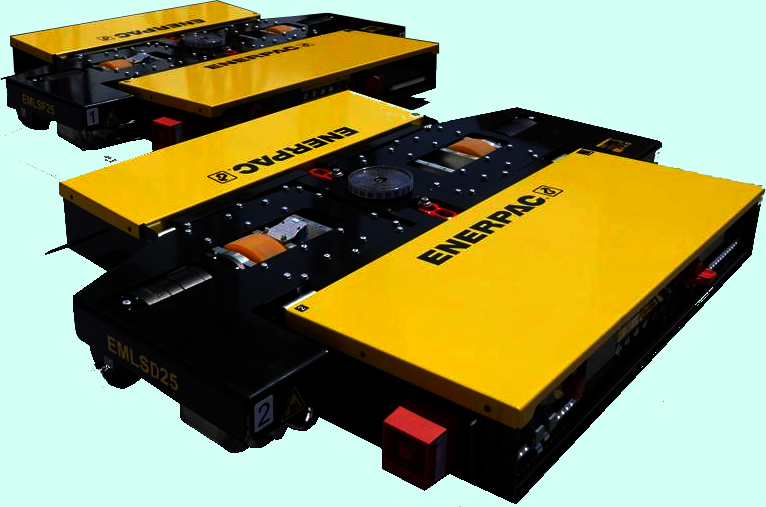
Enerpac announces new Tandem E-Mover Skates for Synchronised Positioning of Bulky Heavy Loads

Enerpac Heavy Lifting Technology has expanded its E-mover skates portfolio with the introduction of the Tandem E-Mover EMLSD25. Operating in tandem pairs, the E-movers are synchronised into a single coordinated system for moving and positioning heavy and bulky loads in confined, low-clearance environments.
At the core of the new E-mover is Enerpac Sync-Drive technology. It utilises a camera-based 360° angle and lifting stroke detection alongside real-time, inter-unit communication across up to four E-Mover EMLSD25s, allowing the E-mover skates to communicate and operate as a unified, highly coordinated transport platform.
“The E-mover EMLSD25 skate enables safe, precise horizontal positioning of large, bulky equipment within confined industrial environments with unmatched control and safety,” says Carsten Daft, Senior Product Manager, Enerpac Heavy Lifting Technology. “Capable of scaling capacities up to 800 kN (80 tons), the integrated E-mover skate features a compact chassis housing drive, steering, lifting, control electronics, and efficient lithium battery power management.”
Advanced Operator Control
The EMLSD25 skate incorporates an integrated 70 mm hydraulic lifting cylinder, enabling operators to safely lift and align loads without high-risk vertical lifting. The remote-control interface features a high-visibility colour display providing live telemetry, including real-time sensor values, load balance, traction, lifting height, and system diagnostics. Battery-powered, the zero-emission EMLSD25 operates quietly with approximately four hours of runtime and fast-recharge capability.
The complete Enerpac E-Mover EMV80SD system includes two E-Mover EMLSD25 skates, two MLSR20B100 follower skates and two remote controls. Operators have the option to use either a single E-mover for smaller jobs up to 500 kN (50 tons) or synchronise both E-movers to increase capacity up to 800 kN for larger, bulkier moves. When using two E-movers, the second remote control provides a monitoring and safety function, for example, when the load obscures the view of the main remote control operator.
Precision Manoeuvrability
Preset functions align multiple E-Movers to a shared coordinate system enabling synchronised tandem movement. In addition, lifting controls are integrated with movement controls for safe incremental raising or lowering of loads with continuous monitoring feedback.
Equipped with dual electric drive motors, gearboxes, and multi-steering modes including zero-radius turning, carousel, crab, and dual-axis steering the EMLSD25 skate can navigate restricted workspaces with extreme precision. Safe operation is built in. Shared safety logic continuously monitors the EMLSD25 skate operating parameters, issuing automatic warnings or halting movement if parameters are exceeded.
For more information on the Enerpac E-Mover EMV80SD system, visit www.enerpac.com
 

Evidence Before Engineering Certainty

By Martin James

For forty years I’ve worked around electrical, instrumentation and control systems, including hazardous areas, ATEX, process environments and industrial automation. One thing has become increasingly obvious to me: the difficult part of using AI in engineering isn't getting an answer. It's knowing whether the evidence actually supports the answer.

AI is becoming remarkably good at finding patterns, generating explanations and producing apparently convincing technical conclusions. But engineering decisions don't happen in a text box. They happen around real assets, real measurements, real operating conditions and real consequences.

That creates a problem. An AI system can look at a dataset and say that a pump is failing. But what does the evidence actually establish? Is the asset correctly identified? Is the measurement relevant? Do we have a trustworthy baseline? Was the equipment operating under comparable conditions? Could there be another explanation? Is the data complete? Has anything been changed since the evidence was collected?

And perhaps most importantly: does the evidence prove the claim, or merely make the claim plausible? These are not the same thing.

Measurement is not proof

I've spent much of my working life dealing with systems where the difference between an indication and a conclusion matters. A transmitter can indicate a condition. A trend can reveal a pattern. An alarm can tell us that something has crossed a threshold. None of those things, by themselves, necessarily establish causation.

Yet when AI is introduced, there is a temptation to move rapidly from data → pattern → explanation → decision. I believe we need another discipline in between: evidence → challenge → contradiction → provenance → decision.

That is one of the ideas behind a system I have been developing called AVAKIMEXA.

AVAKIMEXA

AVAKIMEXA is being developed around a simple proposition: AI can generate a claim. The evidence must decide whether that claim survives.

The system is deliberately positioned at the boundary between machine intelligence and consequential engineering decisions. It does not replace the engineer. It does not take control of the plant. It does not write to PLCs, SCADA, SIS, DCS or actuators. The human remains the authority.

The purpose is different. AVAKIMEXA asks whether the evidence available is sufficient to support the claim being made. Sometimes the answer may be SUPPORTED. Sometimes CONTRADICTED. Sometimes UNRESOLVED. And sometimes the correct engineering answer is simply: INSUFFICIENT EVIDENCE. STOP.

That last answer is important. In engineering, refusing to manufacture certainty can be more valuable than producing another confident prediction.

The evidence obligation belongs to the claim

One principle has become central to my thinking: the evidence required to pass is determined by the claim — not by how convincing the existing evidence appears.

If someone claims that a pump is failing because of bearing degradation, for example, the question isn't whether the available trend looks like bearing degradation. The question is what evidence is actually required to establish that claim.

Asset identity, relevant measurements, operating conditions, baseline behaviour, time relationship, alternative explanations, data provenance, and whatever other evidence is material to that particular claim.

If a material obligation is missing, the system should not quietly fill the gap with confidence. It should expose the gap. That changes the conversation from “What does the AI think?” to “What can we actually prove?”

This matters particularly in safety-critical environments

In hazardous-area and process environments, evidence quality is not an academic issue. An incorrect assumption can influence maintenance, inspection, operational decisions and ultimately safety. The same applies as AI moves further into industrial environments.

We are likely to see increasingly sophisticated systems recommending actions based on increasingly large quantities of data. More data does not automatically mean more proof, and a more sophisticated model does not automatically make incomplete evidence complete.

That is why I think the next stage of industrial AI needs to be less about making machines sound certain and more about making uncertainty visible.

Human authority still matters

There is another boundary I consider non-negotiable. AI should assist engineering judgement. It should not quietly become engineering authority.

The engineer needs to be able to see what evidence was considered; what evidence was missing; what contradictions were found; where provenance matters; what assumptions were made; and why the system stopped or allowed a claim to proceed.

That creates something different from another predictive AI platform. It creates an evidence-adjudication layer between machine intelligence and consequential decisions.

The question I think industry should be asking

We have spent enormous effort asking whether AI can predict, classify, detect and recommend. I think we now need to ask another question: can the AI prove that the evidence it relied upon actually supports the claim it is making?

Because there is a fundamental difference between finding a pattern and proving what caused it. And there is an even bigger difference between generating a recommendation and having sufficient evidence to act on it.

My work on AVAKIMEXA is an attempt to explore that boundary. I am not claiming that AI should replace engineers. Quite the opposite. I am building around the idea that as machine intelligence becomes more capable, human authority becomes more important, not less.

The future industrial AI system may not be the one that gives the fastest answer. It may be the one that knows when the evidence says: Stop. We don't know yet.

Evidence. Not Guesswork.


Hazardous-area maintenance and emergency readiness aboard commercial vessels

Electrical and mechanical equipment aboard commercial vessels can operate in environments where flammable gases or vapours create a risk of fire or explosion. Tankers and vessels carrying certain hazardous cargoes require particularly careful control of equipment installed in classified areas. Shipboard engineers must understand how maintenance activities affect explosion protection while remaining prepared to respond to emergencies at sea. These responsibilities require both technical competence and an understanding of the vessel's safety procedures, particularly when equipment faults arise during a voyage.

Connect hazardous-area maintenance with maritime safety

Equipment maintenance in a hazardous area requires engineers to understand the conditions that could create an ignition source. Electrical inspections may involve checking enclosure integrity, cable entries, earthing arrangements and the condition of components used to maintain an equipment protection concept.

The International Convention on Standards of Training, Certification and Watchkeeping for Seafarers (STCW) establishes minimum international training and competence requirements for seafarers. Relevant STCW courses  develop maritime safety and emergency-response skills that support engineers carrying out their duties aboard commercial vessels.

The convention is maintained by the International Maritime Organization , which establishes an international framework for seafarer competence. Engineers working on vessels with hazardous areas may require additional specialist qualifications appropriate to their technical duties, including training relevant to explosion-protected equipment.

This combination allows personnel to approach maintenance with an understanding of the equipment and the shipboard environment in which the work takes place.

Preserve explosion protection during maintenance

Explosion-protected equipment is designed to prevent ignition under specified operating conditions. Its protective properties can be compromised if maintenance changes the equipment's construction or allows environmental damage to affect critical components.

Engineers should inspect equipment according to the manufacturer's instructions and the applicable explosion-protection standards. Particular attention may be required where vibration, corrosion or repeated maintenance has affected the condition of enclosures and connections.

Replacement components must be suitable for the equipment's certification and intended use. Installing an unsuitable cable gland, modifying an enclosure or replacing a component without considering its protection concept can compromise the original design.

Maintenance records should document the condition of the equipment, work performed and any outstanding defects. This information helps the vessel's engineering team track deterioration and make informed decisions about future inspections.

Maintain control of hazardous-area work

Shipboard maintenance should be planned around the vessel's operating conditions and the potential presence of flammable atmospheres.

Work involving electrical equipment or other potential ignition sources may require specific permits, isolation arrangements and atmospheric testing. The appropriate controls depend on the vessel's hazardous-area classification, the nature of the work and its safety management procedures.

Coordination with the vessel's responsible officers is particularly important when maintenance could affect cargo operations or other activities involving flammable substances.

Prepare engineers for shipboard emergencies

An engineer working aboard a vessel may need to respond to an emergency involving equipment outside their immediate maintenance responsibilities. Fire, flooding or an incident involving hazardous cargo can require personnel to follow established emergency duties under difficult operating conditions.

An STCW basic safety training course  provides foundational preparation for these situations. The training covers personal survival techniques, fire prevention and firefighting, elementary first aid, and personal safety and social responsibilities.

These subjects are especially relevant to personnel whose normal duties involve machinery or electrical equipment. An engineer may recognise an equipment fault during routine maintenance but must also understand how to raise the alarm and respond safely if the situation develops into a wider shipboard emergency.

The training establishes a common foundation for emergency preparedness, while the vessel's safety management system defines the specific actions and responsibilities expected of individual crew members.

Connect equipment faults with emergency procedures

Hazardous-area maintenance and emergency planning should inform one another. A recurring equipment defect may indicate a deterioration mechanism that needs to be addressed before it creates a more serious problem.

Engineers should ensure that significant defects are reported through the vessel's established maintenance and safety procedures. Where an equipment failure could affect fire detection, ventilation or other protective systems, the implications for continued operation should be assessed before work proceeds.

Emergency exercises provide an opportunity to understand how technical failures could influence the crew's response. An engineer familiar with the vessel's electrical distribution and machinery arrangements can contribute useful information about equipment isolation and the restoration of essential services.

Maintain technical competence and emergency readiness together

Safe maintenance aboard vessels with hazardous areas depends on correctly maintained equipment, competent personnel and effective operational controls.

Engineers need to preserve the protective properties of equipment during maintenance while understanding their responsibilities within the vessel's emergency arrangements. Integrating technical inspections with maritime safety training and established reporting procedures helps crews identify developing hazards and respond appropriately when equipment problems affect shipboard safety.

New Encapsulation Rules: What Changes for Your Ex Design?

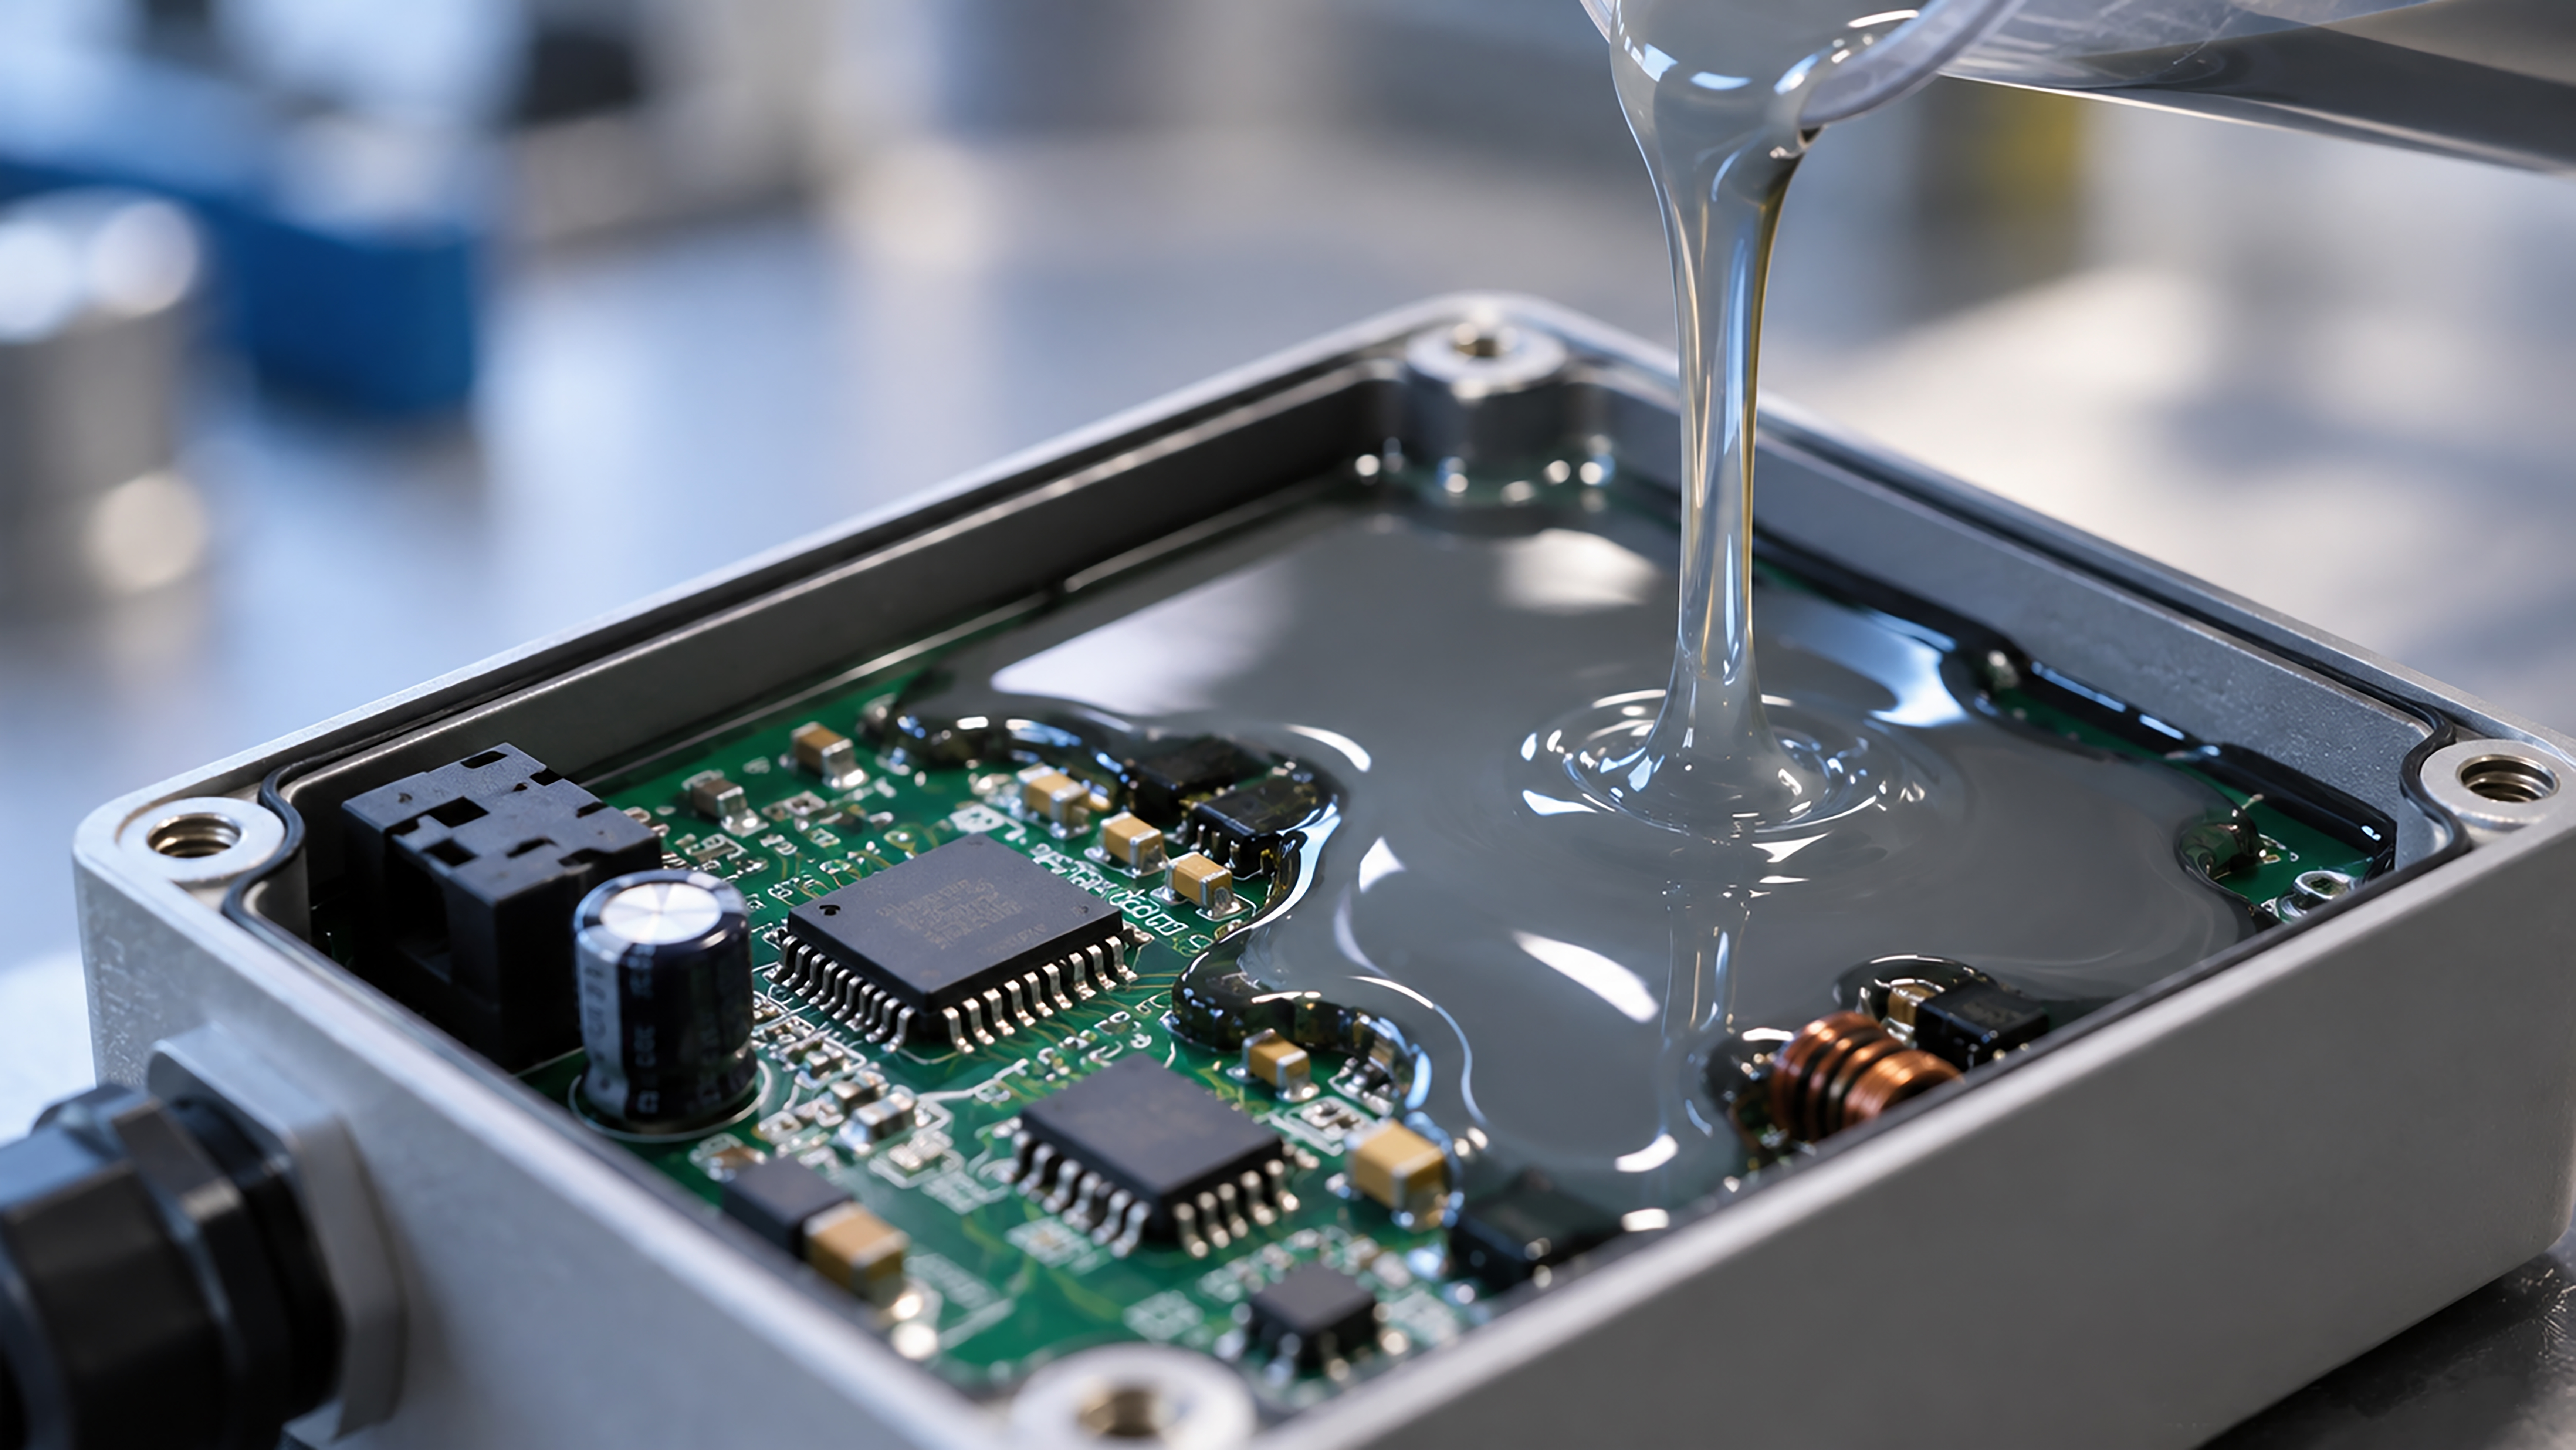
Encapsulation protection, or “m”, is a protection technique used to prevent ignition in equipment for explosive atmospheres across oil and gas, mining and other industrial applications.

For over 10 years, manufacturers of encapsulated equipment for explosive atmospheres have worked to IEC 60079-18:2014 and its subsequent amendment. IEC 60079-18:2025, Edition 5.0, is the first full technical revision of the encapsulation “m” standard since then.

While the fundamental protection concept remains unchanged, Edition 5 introduces four Major Technical Changes. For manufacturers, the important question is not simply what has changed, but which changes could affect existing products, new designs and future certification.

Where are the significant changes?

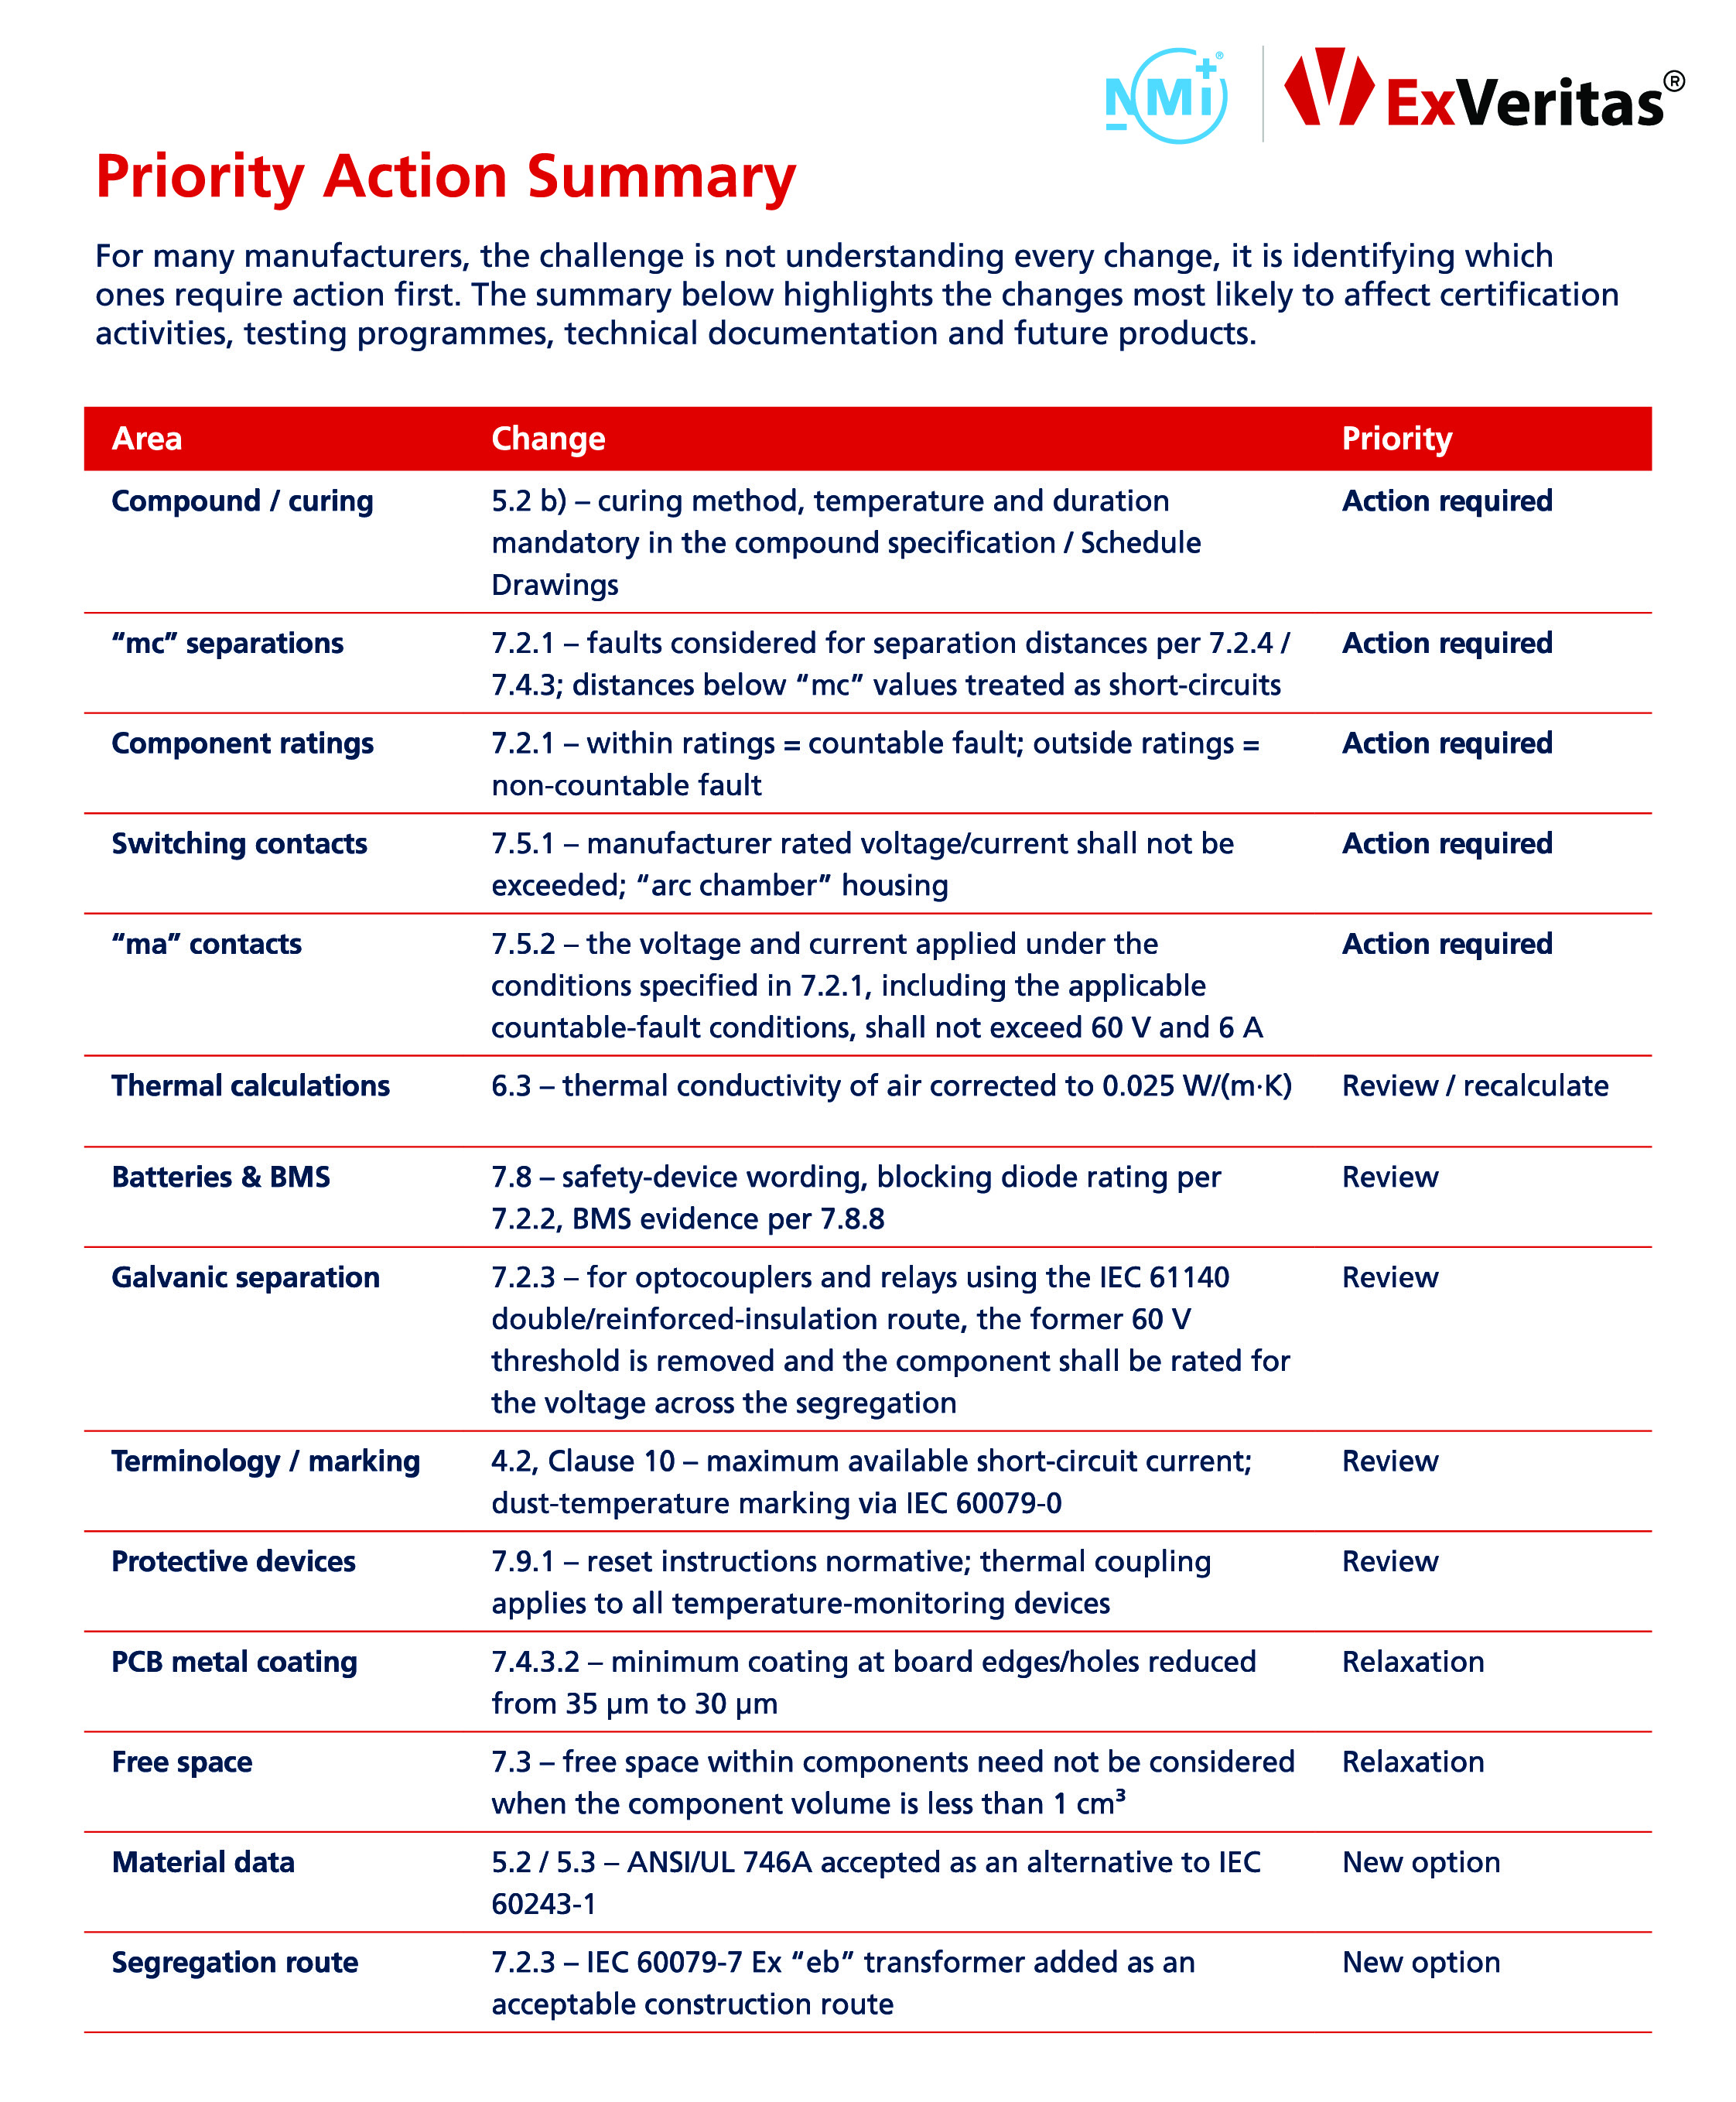
The following areas deserve attention first because they include the Major Technical Changes and other changes with significant practical impact on the design and certification of encapsulated equipment.

Compound specification and curing

Edition 5 requires the curing method, temperature and duration to be included within the controlled compound specification.

This makes curing conditions an explicitly controlled part of the design and manufacturing process. Manufacturers should consider whether this information is already adequately captured within their controlled documentation. Where curing conditions are recorded elsewhere, documentation updates may be required.

Fault examination for “mc”

Edition 5 expressly applies the relevant separation-distance requirements to “mc”. Compact designs therefore cannot disregard these requirements simply because faults are generally not considered for “mc”.

Component fault treatment is also clarified. A component operating within its manufacturer ratings is treated as a countable fault, while operation outside those ratings is treated as a non-countable fault.

For compact “mc” equipment or designs relying on highly-stressed components, these provisions warrant particular attention.

Encapsulated switching contacts

The rated voltage and current specified by the switching-contact manufacturer must not be exceeded, while the housing around the arcing area is now termed the “arc chamber”.

For Level of Protection “ma”, the 60 V and 6 A limits must also be met under the applicable fault conditions specified by the standard. Manufacturers of “ma” equipment incorporating switching contacts should therefore verify the voltage and current under these conditions, rather than considering normal operating values alone.

Thermal calculations and battery systems

The previous edition included a note giving the thermal conductivity of air as 0.25 W/(m·K). This has been corrected to 0.025 W/(m·K).

Where the previous value was used to determine the hottest component or compound temperature, the calculation should be reviewed and, where necessary, recalculated.

Battery-powered equipment also receives additional attention.

The term “control device” is generally replaced by “safety device”, while Edition 5 introduces more explicit responsibilities where a Battery Management System provides a protection required by IEC 60079-18.

Evidence is required that the BMS remains functional under the expected relevant malfunctions. The equipment manufacturer should retain the appropriate supporting declaration from the BMS manufacturer and include information necessary to maintain the integrity of the protection within the product instructions.

Blocking diodes used to prevent reverse current are also subject to specified rating requirements.

ExVeritas September HES Content Image 2 PRINT

What should manufacturers do now?

A structured gap assessment remains the clearest way to separate substantive technical gaps from changes with little practical impact, particularly for "mc" designs, "ma" switching contacts, and battery systems affected by the BMS provisions.

NMi ExVeritas carries out these assessments for encapsulated equipment manufacturers, mapping Edition 5 requirements against existing designs and documentation ahead of transition and certification deadlines.

https://www.exveritas.com/

Intrinsically Safe Ultrasonic Sensors for Hazardous Environments

In industries such as oil and gas, chemical processing, mining, energy, food and beverage, and material handling, measurement equipment is often required to operate where flammable gases, vapors, or combustible dust may be present. In these environments, selecting the right sensor is not only about measurement performance. It is also part of the overall safety strategy.

Intrinsic safety is an explosion-protection method that limits the electrical and thermal energy available within a circuit, helping prevent the ignition of a potentially explosive atmosphere. When properly installed with an approved intrinsic safety barrier, an intrinsically safe ultrasonic sensor can provide non-contact level and distance measurement within hazardous areas.

This makes ultrasonic sensing particularly useful for applications such as monitoring flammable liquid levels in tanks, measuring material levels, detecting objects or equipment position, and monitoring distance on process equipment. Because ultrasonic sensors operate without contacting the target material, they can also reduce exposure of the sensor to corrosive, abrasive, or otherwise difficult materials.

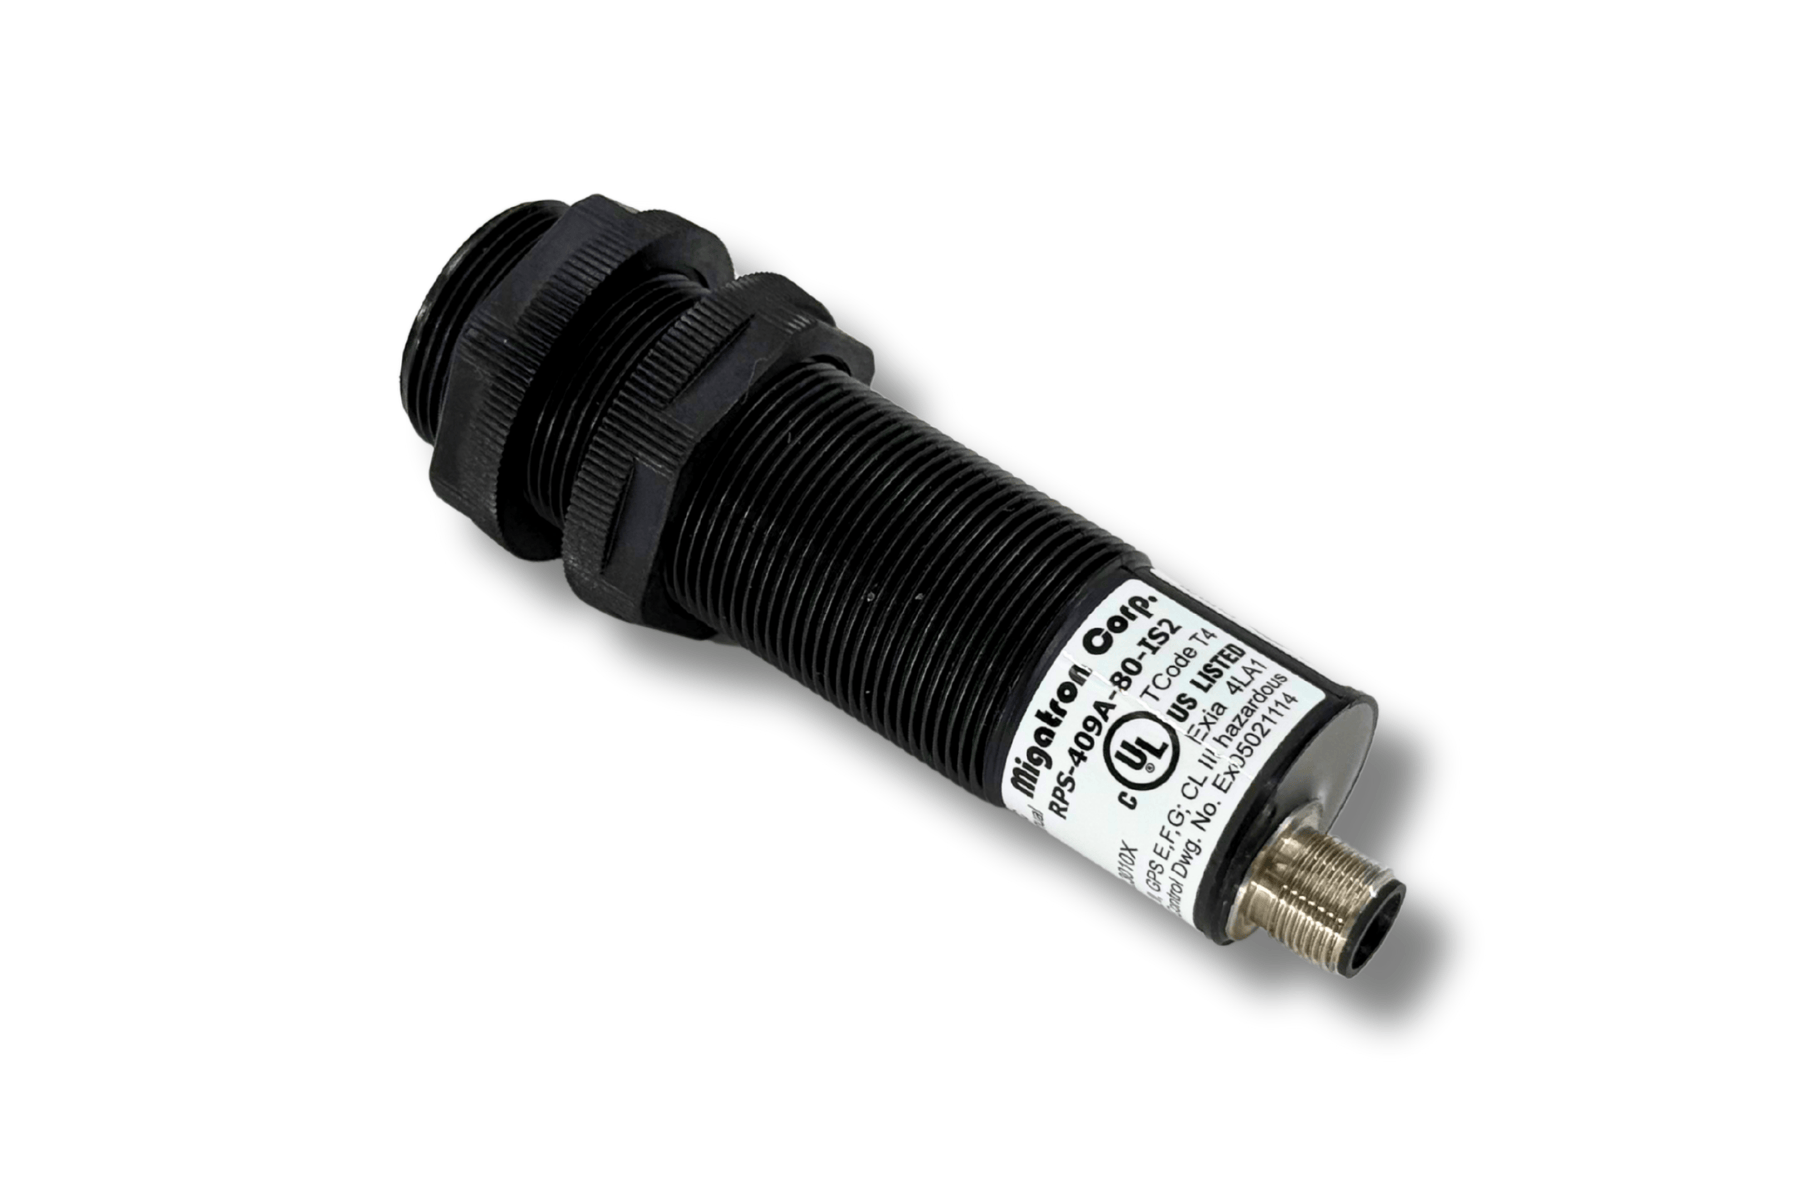
Migatron Corporation designs and manufactures intrinsically safe ultrasonic sensors for hazardous area applications. The RPS-409A-IS2 carries ANZEx, ATEX, IECEx, and C-UL-US approvals and is designed for use in mines susceptible to firedamp (Group 1 protection level Ma), and in hazardous gas and dust environments, including Zones 0, 1, 2, 20, 21, and 22 and Class I, II, and III locations when used with an approved intrinsic safety barrier(s). The RPS-429A-IS also offers ATEX, IECEx, and C-UL-US approvals, with 4–20 mA current-loop or 1–5 V analog output options.

As automation expands into hazardous environments, safe and reliable measurement becomes increasingly important. Migatron also works directly with OEMs and engineers to develop customized ultrasonic sensing solutions tailored to specific application and integration requirements.

http://www.migatron.com/

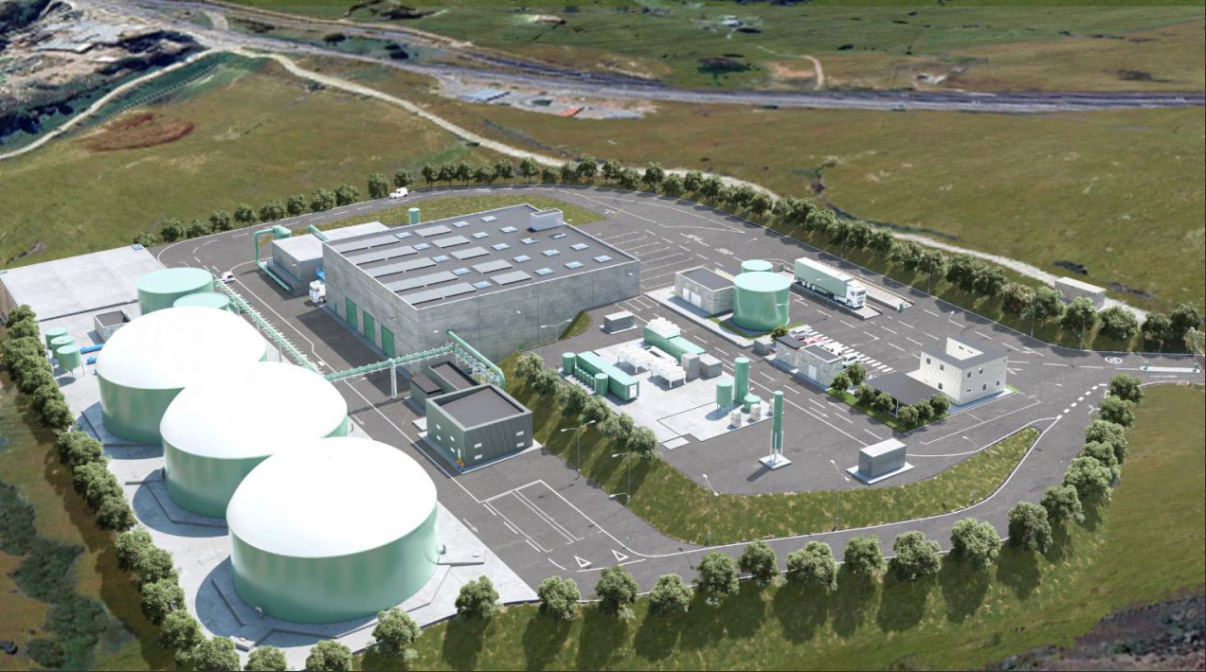
WELTEC BIOPOWER has begun construction of a new biomethane plant in Colmenar Viejo, north of Madrid, alongside environmental services provider PreZero and Enagás Renovable.

weltec_3.jpeg

Once operational, the facility will generate up to 60 GWh of renewable energy annually, enough to meet the energy requirements of approximately 11,700 households or 30,000 residents.

The plant will process up to 75,000 tonnes of organic waste each year, including separately collected household biowaste from Colmenar Viejo and surrounding municipalities. Rather than being sent to landfill, the organic material will be converted into renewable biomethane.

At the heart of the facility will be three stainless-steel digesters supplied by WELTEC BIOPOWER. Each digester measures 25.34 metres in diameter and 10.05 metres in height, with a capacity of 5,067 cubic metres. A gas-tight pre-storage tank will help maintain a continuous substrate supply and stable operating conditions.

“Stainless steel is particularly resistant to corrosion under the demanding biological and chemical conditions found in the digestion process. This gives the plant a long service life, high operational reliability and low maintenance requirements,” said Alain Priser, International Sales Manager at WELTEC BIOPOWER.

The facility will operate as a closed and sealed system, with biofilters and activated carbon systems designed to remove up to 99% of odorous substances from exhaust air. The resulting biomethane will be injected directly into the gas grid.

The project is expected to contribute to Madrid's efforts to reduce landfill use while converting regional organic waste into locally produced renewable energy.

WELTEC BIOPOWER will provide further information about the technology at stand 276A at Salon del Gas Renovable in Valladolid, 29–30 September 2026.

ABB expands hazardous-area dust monitoring with new PFM 20 Ex

ABB has expanded its industrial emissions measurement portfolio with the launch of the PFM 20 Ex, a new dust monitoring device developed for use in hazardous and harsh industrial environments.

Designed for applications where robust equipment and low-range measurement are essential, the PFM 20 Ex provides a certified dust detection range down to 7.5 mg/m³ and meets ATEX Zone 22 certification requirements.

The new device extends ABB’s dust monitoring capabilities and forms part of the company’s wider industrial emissions measurement offering, which includes continuous emissions monitoring, particulate analysis, dust and gas flow measurement and portable hydrocarbon detection.

The launch also builds on the measurement technologies added to ABB’s portfolio following its acquisition of Födisch Group in 2024. The acquisition expanded ABB’s capabilities in dust and gas flow measurement as well as portable hydrocarbon detection.

By bringing these technologies together, ABB says industrial operators can source a broader range of emissions measurement solutions from a single supplier, helping to simplify supplier coordination and provide a more consistent approach to selecting, deploying and supporting measurement equipment across industrial facilities.

“The PFM 20 Ex is an important product launch in its own right, giving customers high-sensitivity dust monitoring for hazardous environments,” said Jean-Rene Roy, Global Business Line Manager at ABB’s Measurement & Analytics division.

“This also represents a significant addition to our highly capable industrial emission measurement portfolio, enabling us to support a broader range of customer needs, from continuous gas analysis to dust, gas flow and portable measurement.”

ABB’s industrial emissions measurement portfolio includes continuous emission monitoring systems such as the ACF5000 and MCA 10 CEMS, alongside particulate analysers including the PFM 20, PFM 13 and OPM 19 ED dust analysers. The range also incorporates the FMD 09 gas flow analyser and portable Flame Ionisation Detectors (FIDs) for real-time, on-site hydrocarbon detection.

The measurement technologies are supported by remote and on-site service capabilities and flexible care agreements. ABB’s My Measurement Assistant+ (MMA+) also provides users with access to device health information, reports, documentation and AI-powered device-specific knowledge and support.

With the addition of the PFM 20 Ex, ABB is extending its ability to support industrial operators requiring dust and emissions monitoring technologies suitable for demanding and potentially hazardous operating environments.