Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

News

Rethinking Device Lifecycles in Hazardous Areas

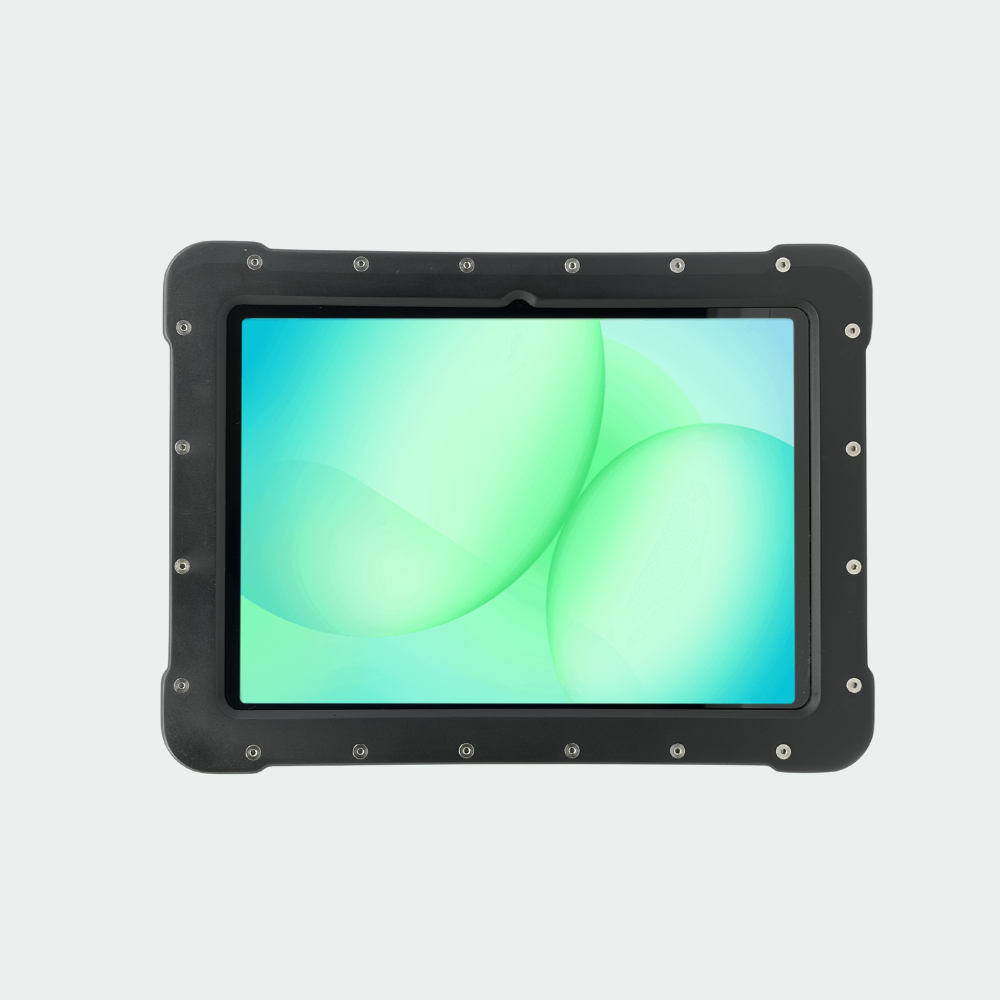
In hazardous areas, mobile devices are subject to strict certification requirements. This directly affects how equipment is selected and replaced. In practice, there are two common approaches. The first is fully certified Ex tablets. These are intrinsically safe devices where the certification is built into the hardware itself. The second approach uses standard consumer tablets combined with a dedicated explosion-proof enclosure. Despite their differences, both approaches share the same limitation. The device and the explosion protection are effectively locked together. When the hardware becomes outdated, underpowered, or unsupported, the entire solution must be replaced.

inlay system

For Ex tablets, this is because the certification is tied to that specific device. You cannot upgrade internal components without invalidating certification. For consumer tablets with Ex housings, the enclosure is designed for one specific model. Once that tablet is ready for an upgrade, the enclosure can no longer be reused. In both cases, a hardware refresh results in full replacement, including components that are still mechanically sound.

A More Sustainable Approach A more sustainable model separates the device from the explosion protection. Instead of treating them as a single unit, they become modular components. In this setup, the enclosure remains a long-term asset, while the tablet inside can be upgraded independently. This allows companies to follow standard IT lifecycles without replacing the certified housing each time.

It also removes a common bottleneck. With traditional Ex devices, users often have to wait for new certified models to access updated technology. A modular approach allows immediate use of newer consumer hardware, without being dependent on certification cycles. The result is a system that is both more flexible and more aligned with modern expectations around sustainability and cost control.

A Universal Modular Solution The UniCase by Armadex is built around this modular principle. Instead of being tied to a single device, the enclosure is designed to work with multiple tablet models through an interchangeable inlay system. The outer housing remains unchanged, while the inlays are tailored to a specific device. Buttons, touchscreen, cameras, and microphones can be used as intended, without compromising usability.

When upgrading to a new tablet, only the inlay and the device are replaced. The enclosure itself is reused. This approach decouples the lifecycle of the ATEX tablet enclosure from that of the device, while maintaining full operational functionality in the field. Looking Ahead As industries place more emphasis on sustainability and efficiency, the way equipment is designed and managed becomes increasingly important.

A modular system allows companies to reduce waste by reusing durable components. It also avoids repeated investment in certified housings, which is the most expensive part of the solution. At the same time, it ensures access to the latest technology. Devices can be upgraded when needed, without waiting for new certified variants or replacing the entire setup. In hazardous environments, where reliability and compliance are essential, this approach provides a more balanced model. It supports long-term use of costly certified equipment while enabling continuous technological improvement.

Why CHEMUK has become the heartbeat of the UK chemical supply chain

chemuk.jpeg

CHEMUK returns to the NEC, Birmingham, on 20 May and 21 May as the UK’s largest event dedicated to the full chemical supply chain. With the sector undergoing rapid transformation driven by innovation, evolving regulation and the pressure to deliver more resilient, sustainable operations, it is vital for manufacturers, suppliers, formulators and logistics leaders to use this rare opportunity to access every part of the industry ecosystem under one roof.

Described by Tim Doggett, CEO of the Chemical Business Association (CBA), as the “go-to event of its kind in the UK, and arguably even in Europe, for the complete chemical supply chain”, CHEMUK brings delegates from across the UK and further afield for two days centred on creativity, collaboration and innovation. What really makes the event special is its community. It has a unique ability to bring together the whole chemical supply chain, combining a strong exhibition with a high-quality conference programme and keeping people at the heart of the experience.

Across its expanding show zones, CHEMUK presents over 600 specialist exhibitors representing raw materials, ingredients, intermediates, specialty chemicals, process technologies, engineering solutions, packaging, handling, distribution, waste management and regulatory compliance. This breadth is what sets the event apart: it is not just a marketplace for products, but a cross-section of the UK’s chemical value chain. Whether you are sourcing critical inputs, improving production efficiency, reviewing safety solutions or exploring the latest in green chemistry, the event provides direct access to the partners and technologies shaping the sector’s future.

For operations, supply chain and compliance professionals, CHEMUK offers clear and immediate value. The Chemicals Management and Process & Chemical Engineering zones provide practical insights into improving safety, reducing operational risk and meeting tightening regulatory requirements. Exhibitors demonstrate advancements in hazard mitigation, labelling, transport, storage, automation, data management, emissions monitoring and waste-to-resource processes.

Upstream and downstream players benefit equally. Raw material suppliers connect with formulators and brand owners through the Chemicals Supply Show and the Formulated Product Manufacture Show, enabling efficient sourcing, faster product development and stronger supplier–customer integration. For R&D teams and analytical specialists, the Chemicals Laboratory Show brings together the latest laboratory technologies, instrumentation, testing services and analytical solutions.

Alongside the exhibition, the CHEMUK 2026 conference programme brings together expert speakers from across industry, government, academia and the wider chemicals. 

ecosystem to address the most pressing strategic and technical issues facing the sector. Spanning multiple theatres across the two days, sessions will cover themes such as regulatory change, chemicals management, decarbonisation, digitalisation, circularity and innovation in formulated products. Case studies, panel discussions and technical talks will help attendees benchmark strategies, learn from peers and take away practical ideas they can apply in their own organisations.

CHEMUK 2026 will take place in Hall 5 at the NEC and is free to attend for industry professionals. Running from 09:30–17:00 on 20 May and 09:30–16:00 on 21 May, the format is designed to maximise networking while allowing delegates to combine supplier meetings with conference sessions and feature areas.

In a sector where efficiency, safety and innovation are inseparable, CHEMUK has become a cornerstone event and a catalyst for collaboration. For leaders across the full supply chain, it is where the industry unites to solve today’s challenges and shape tomorrow’s opportunities.

Fast Ex-p compressor motor for zone 1 – availability meets explosive atmosphere expertise

menzel_gmbh.jpeg

In just three weeks, MENZEL delivered a water-cooled, pressure-encapsulated (Ex-p) compressor motor to Austria’s largest plastics manufacturer. This was possible because both the base motor and the required Ex-p system were available from stock, and we have the expertise to convert standard motors to Ex-p in-house, TÜV-certified.

Challenge: High safety requirements with minimal lead time

The customer urgently required a replacement for a compressor drive operating in a hazardous area (Zone 1). In addition to complying with the protection class II 3G Ex pzc IIB T3 Gc, fast availability was critical, as the compressor plays a key role in the production process. The new motor had to fit exactly into the existing footprint, including foundation dimensions, flange positions, and connection geometries.

All necessary modifications to the stock motor had to be completed within three weeks. MENZEL engineers were on-site even before order placement to review the installation situation and clarify all technical details.

Solution: Perfect combination of stock availability, engineering expertise, and Ex-p know-how

MENZEL successfully executed the project because both the suitable squirrel-cage motor from the MEBKSW series and the pressure-encapsulated Ex-p system were immediately available from stock – a decisive advantage over many other manufacturers.

The stock motor was extensively adapted to the application and installation site. The housing was equipped with purge flanges, allowing the motor to be flushed with a non-ignitable gas mixture before start-up, while overpressure during operation prevents the ingress of hazardous gases. The motor was certified II 3G Ex pzc IIB T3 Gc, and all testing according to applicable Ex standards was performed in our in-house certified test facility.

Additional modifications included:

  • Conversion to cooling type IC 81W (water-cooled)
  • Mechanical adjustment of frame size from 560 to 630
  • Relocation of terminal boxes
  • Preparation of the star-point terminal box for current transformers
  • Adjustment of bearing flange connections
  • Installation of vibration sensors

Thanks to close cooperation between engineering, manufacturing, and quality assurance, all mechanical and electrical work was completed within three weeks and delivered via special truck. MENZEL also offered technical supervision for commissioning.

Contact:

Menzel Elektromotoren GmbH

Am Alten Walzwerk 2

16761 Hennigsdorf, Germany

Phone: +49 30 349 922-0

Email: This email address is being protected from spambots. You need JavaScript enabled to view it.

Internet: www.menzel-motors.com

Intrinsic Safety without compromise

esi_march_19.jpeg

When hazardous environments demand absolute confidence, ESI Technology’s ATEX and IECEx certified pressure transducers and pressure transmitters deliver proven performance without limiting application choice. Across industries where explosive atmospheres, extreme pressures and harsh conditions are the norm, ESI provides intrinsically safe versions of pressure measurement solutions tailored to hundreds of real-world applications.

The range covers an exceptional breadth of measurement requirements, including high pressure, low pressure, differential pressure, and high-accuracy instruments, alongside specialist options such as subsea-rated designs and flush membrane versions for viscous, corrosive or hygienic media. Whether monitoring minute pressure changes or operating reliably under extreme pressure loads, ESI ensures intrinsic safety is never a constraint on performance.

Designed and manufactured in North Wales, ESI’s intrinsically safe products combine robust mechanical construction with advanced sensor technologies, including Silicon-on-Sapphire, delivering long-term stability, excellent temperature performance and outstanding resistance to harsh process conditions. ATEX and IECEx approvals allow confident deployment in Zone 0, Zone 1 and Zone 2 environments, supporting global compliance across oil and gas, chemical processing, marine, hydrogen, mining, aerospace and general industrial applications.

dust.jpeg

Crucially, intrinsic safety at ESI is not an afterthought. Many standard product platforms are available with intrinsically safe variants, enabling engineers to select the right pressure range, accuracy level, output signal and mechanical interface without redesigning systems or compromising on specification.

From offshore platforms and subsea installations to processing plants and hazardous manufacturing environments, ESI Technology offers an intrinsically safe pressure solution to match the application, not the other way around.

If your application operates where safety is critical and performance cannot be compromised, there is likely an ESI intrinsically safe solution engineered to fit.

Dräger expands multi-gas detector functionality with covert feature for high risk operations

drager_march_2026.jpeg

Dräger, an international leader in medical and safety technology, has expanded the functionality of its Dräger X-am 8000 multi-gas detector with a covert feature that allows users to silence audible and visual alerts to maintain mission-critical operational discretion and safety. 

Able to identify up to seven gases at once, the X-am 8000 detects toxic and flammable gases as well as vapours and oxygen. It uses either a pump, where the device actively draws air from a specific location through a hose or probe, or the lower-power diffusion mode where gases naturally diffuse into the sensors of the device without mechanical assistance. Suitable for various applications, the X-am 8000 can be used for personal air monitoring, confined space entry, and area monitoring. 

Designed specifically for military, police, and special operations users, the new Stealth Mode feature helps to prevent alerts from revealing personnel positions during frontline deployments or covert operations.  

Stealth Mode can be enabled using Dräger’s supporting gas detection CC Vision software (version 7.5.3 or later) and exists in addition to temporary muting via the device menu or permanent muting via CC Vision. 

Tom Pearson, Marketing Manager, Engineered Solutions and Government Agencies at Dräger, says this feature is a critical component of Dräger’s defence and security capabilities:  


“At Dräger, we work in partnership with contractors and end users to ensure that our technology can fit their application requirements so that they can carry out their jobs with confidence. 


“By working closely with the military, government agencies, emergency services and other special forces, we know the dangers that these professionals face daily. 

“Discretion and safety go hand in hand during high-risk situations. For military and police personnel, remaining covert is vital. Being able to operate on the frontlines without triggering audio or visual disruptions allows users to go unseen, which could be lifesaving.” 

To find out more about the X-am 8000 and Stealth Mode for police and military applications, visit: https://www.draeger.com/en_uk/Contact 

MTX 3297 Ex – Certified for Zone 0 Environments

In industries such as chemical plants, pharmaceutical production facilities, oil refineries and mining - precision, reliability, and safety are paramount! The MTX 3297 Ex digital multimeter from Chauvin Arnoux is built to improve how professionals work in explosive atmospheres.

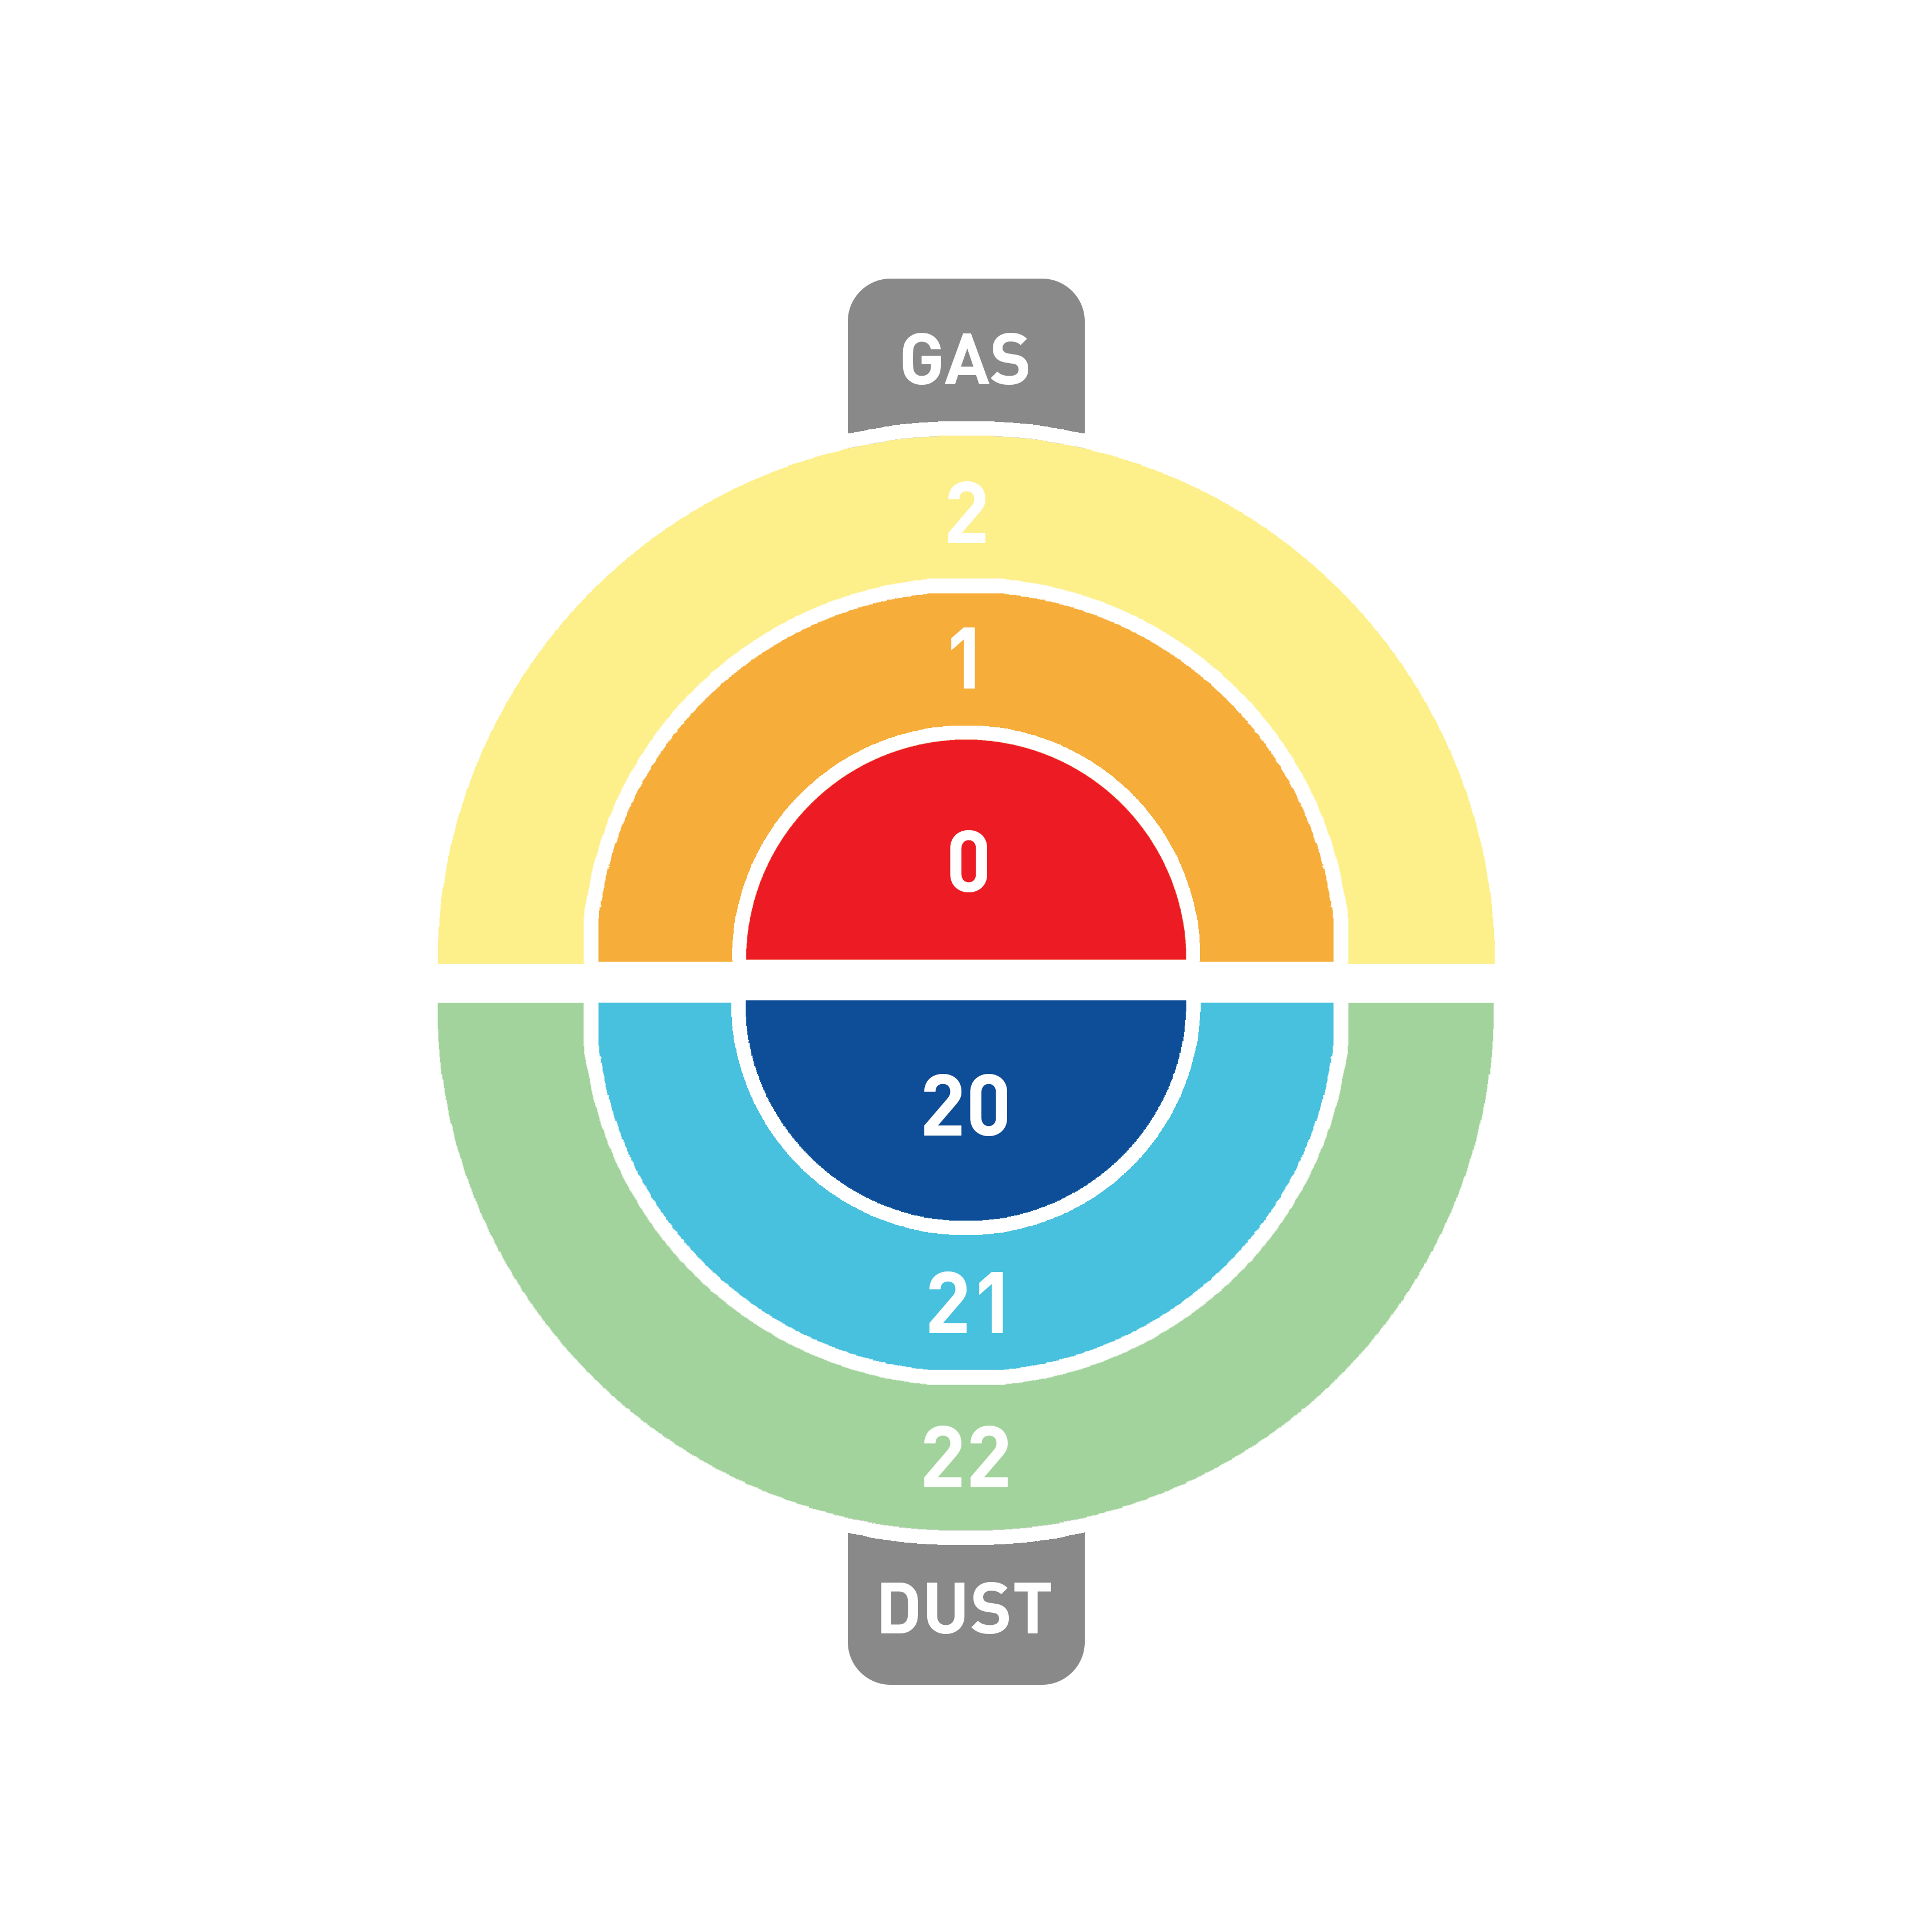
Certified under European directive 2014/34/UE, it meets strict safety standards for hazardous zones, including gas zones (0, 1, 2), dust zones (20, 21, 22), and M1 mining applications. This allows technicians to perform essential tests and troubleshoot with certainty and reduced risk. But offering safety is just the starting point!

Maintenance teams face increasingly difficult challenges, for example, dealing with stray voltages, fluctuating signals, and the need to quickly pinpoint faults in high-risk industrial systems. The MTX 3297 Ex offers advanced measurement capabilities, including low-impedance voltage readings and a low-pass filter for PWM signals, which minimise interference and provide accuracy in tough environments. Its features, such as Min/Max, Peak, and differential measurements, enable specialists to perform detailed diagnostics, quickly identify anomalies, and make informed decisions to prevent equipment failures.

This digital multimeter stands out for its detailed measurement capabilities! Its broad range, including capacitance measurement and extended frequency coverage, makes it suitable for a range of industrial applications. For businesses, this leads to faster problem-solving, improved reliability, and reduced downtime.

The dual display allows users to view two measurements simultaneously, reducing mode changes and enabling technicians to identify issues more quickly. This saves time, eliminates errors, and streamlines maintenance tasks.

The MTX 3297 Ex is also built for use in harsh industrial conditions. With an IP67 rating, it is protected against dust and can withstand exposure to water, making it reliable in dusty, wet, or tough environments. Its high safety ratings (1000 V CAT III / 600 V CAT IV) mean it The CAT rating indicates suitability for specific electrical zones. CAT III applies to distribution-level equipment with lower fault currents protected by miniature circuit breakers (MCBs) and is used downstream of the incoming fuse. CAT IV is intended for use upstream of the distribution board (DB) for utility operations and/or systems.)

For companies operating in hazardous environments, the MTX 3297 Ex improves safety, enables faster, more accurate fault detection, and helps preserve seamless equipment

 [RL1]Hope this reads right? Please leave your suggestion in comments - if it should be tweaked

 [GU2]Hi Rochel, everything looks great. The sentence is technically correct - the CAT rating means it can be used in different electrical zones CAT III can be used at distribution level equipment where fault currents are lower as they have MCBs you can use CATIII anywhere down stream of incoming fuse - CAT IV can be used upstream of the DB on electrical utilities side. Hope this helps

operation. Visit www.cauk.net to learn more or book a free demonstration. (398/400

Explosion Proof ATEX/IECEx Zone 1 / 21 iPhone 17

Atexxo introducing the ATEX iPhone 17 – Certified Communication for Hazardous Environments

  atexxo_3.jpeg                              


 iPhone 17 for ATEX Zone 1 / 21                                iPhone 17 for ATEX Zone 2 / 22

Introducing the ATEX iPhone 17 – Certified Communication for Hazardous Environments

Professionals working in hazardous areas no longer have to choose between safety and cutting-edge technology. The new ATEX iPhone 17 Zone 1 / 21 brings the latest Apple performance to industries where explosive atmospheres are part of daily operations.

Designed for use in ATEX Zone 1 (gas) and Zone 21 (dust) environments, the device is engineered and certified to operate safely in locations such as oil & gas facilities, chemical plants, offshore platforms, grain processing plants, and pharmaceutical production sites. The ATEX modification ensures that the smartphone meets strict European explosion-safety requirements while preserving the full functionality users expect from the latest iPhone.

The ATEX iPhone 17 combines Apple’s powerful hardware with specialized safety engineering. The device is housed in a robust protective enclosure designed to prevent ignition risks while maintaining usability in demanding industrial settings. All electrical components are carefully integrated and protected according to ATEX certification standards, ensuring safe operation in environments where flammable gases or combustible dust may be present.

Despite its ruggedized safety design, the smartphone retains the premium experience of the standard iPhone 17. Users benefit from a high-performance processor, advanced camera system, large high-resolution display, and seamless connectivity. This makes the device ideal for modern industrial workflows, including digital inspections, remote expert support, video documentation, asset management, and industrial communication apps.

The ATEX iPhone 17 is also designed for practical use in the field. The enclosure offers enhanced durability, improved grip for gloved operation, and reliable protection against dust and moisture, allowing workers to operate confidently in challenging environments. The device supports the latest enterprise mobility solutions, ensuring smooth integration into existing IT and security infrastructures.

By combining Apple innovation with certified explosion protection, the ATEX iPhone 17 provides a future-ready communication platform for hazardous industries. Workers gain access to powerful mobile technology without compromising on safety or compliance.

The result is a smartphone that enables smarter workflows, improved safety, and greater productivity in environments where reliability and certification are critical. ATEX iPhone 17 – The power of Apple technology, engineered for hazardous areas.
For more information, please visit www.atexxo.com

Controlling dust in production

Nicolas Van der veken, Product Manager at Donaldson

Effective dust control can support optimal working conditions, as well as compliance with dust emissions standards and regulations, and can help mitigate risks associated with combustible dust*.

For effective dust control filter efficiency is often the focus, while two other key factors – exposure and emissions – are commonly overlooked. Failing to consider these two elements can mean that dust control performance is not fully optimised.

A qualified industrial hygienist can audit a facility to evaluate air quality and potential employee exposures, determining average or peak concentrations of contaminants. Hooding can be an effective means of reducing exposure to dust, which should be designed effectively and properly located near the dust generation source. An audit can identify the facility’s dust sources to verify if ventilation hooding currently in use is appropriate. This is often when new dust generation points and the need to add controls, such as additional hood locations, are identified.

Once exposure areas have been addressed, the next step is to review appropriate dust collection technology. A dust collector should deliver consistent and predictable performance that effectively removes contaminants, while maintaining a consistent air volume at a predictable energy cost.

When assessing the appropriate dust collector, is also important to carefully analyse the type of filter and its efficiency. A filter in a regenerative dust collector is often pulse-cleaned under heavy loads. It must handle new dust entering the collector, in addition to all the dust accumulated on it over time. Evaluating a dust collector in terms of what it achieves at its stable set point, and using exposure and emissions testing will give a better indication of the ventilation system’s performance.

Outlet emissions are what ultimately passes through the dust collector. It is therefore important to know the quality of the filtered air being emitted back into the building or exhausting outside. This requires systematic testing to monitor air quality. For some facilities, industry-relevant regulations mandate continuous emissions monitoring. Other local and international standards may also apply, dictating the need for a variety of test methods to determine emissions or exposure limits.

Once ventilation needs and emissions limits are understood, a qualified industrial ventilation designer can design a dust collection system. They will identify what the dust load demands may produce in terms of energy and cleaning consumption, and how to achieve emissions goals in both a cost and energy efficient way.

Effective dust management can help prevent airborne particle contamination during manufacturing, support product quality consistency, and reduce production interruptions from contamination problems. Dust filtration can also help protect equipment, as well as contribute towards prolonging machinery life and overall system performance. Additionally, extended filter longevity can minimise operational downtime, while reduced air consumption can support lower long-term operational and energy costs. Taking into consideration dust collection in terms of exposure, efficiency and emissions will support the optimisation of dust control performance throughout the production process.

Contact Donaldson for expert support with your dust control challenges


Donaldson Blue On White Horizontal tag660

Hart’s success with its range of doors

Writes Chris Dobson

 Working through a major developer which delivers high-profile infrastructure projects, Hart Door Systems has supplied 16 industrial doors, ranging from  Speedor Storms to insulated shutters for a major Waste Transfer Station.  

Hart’s chairman, Doug Hart says the scheme is billed as a step forward into a greener future and “we are delighted to be part of this significant project which demonstrates our broad range of industrial door products”.  

He adds: “Time and again clients tell us Speedor Storm is chosen because of its fast open and close operation. This in turn helps with environmental control and energy use reduction, essential for any major green project. Other Speedor Storm benefits include reliability and technologically advanced features which boost efficiency.”

Hart Door System’s wind-resistant, high-speed, industrial rolling door, Speedor Storm, is ready for business be it a factory, warehouse, storage facility or any kind of plant operation that has one or more large external openings which must be opened frequently for people and traffic.

With wind resistance available up to ‘wind class 5’, as defined by DIN EN 12424, in the closed position this high-speed door is ready for openings to a maximum 8 metres width or height subject to 48 square metres. This ability to withstand substantial wind pressure means major entrances open/close automatically so avoiding a less than optimal working environment and the escape of heated air.

Speedor Storm is designed specifically to help with several areas of business notably productivity, improving environment in which to work, delivering maintenance of temperature and environment by door preventing penetration by wind born debris.

Made at Hart’s Newcastle factory, from where its teams of engineers are available throughout the UK for installation and reliable servicing and maintenance thereafter.

The benefits of Speedor Storm come from its unique guide system in combination with other carefully designed features. Further Speedor Storm’s strength and wind resistance comes from its multi-layer PVC and textile, both long-lasting and tear-resistant and its inbuilt horizontal curtain braces and no external cumbersome and noisy external wind bars.

There is a colour choice as well as ‘a with or without vision panel ’ which combine to deliver a good appearance, operational effectiveness and a performance product.

Safety features include a state of the art safety light curtain, anti-fall protection and sensors to activate the door. There is a range of operating methods that include hands free, floor loops, radar, photo beam, radio operation, movement sensors, handheld or vehicle-mounted radio transmitters,  or simple push button and pull cords.

The automatic operation can be set to include or exclude pedestrians as desired. If warning lights or klaxons are required, these can be incorporated in a complete door system and control panel which are designed for any conceivable need including integration into a Building Management System if necessary. This is delivered via its unique guide system in combination with other carefully designed features.

Little wonder Speedor Storms are so highly regarded.

www.hartdoors.com

UK First: Element Achieves Nationally Recognized Testing Laboratory (NRTL) Status to Deliver Direct Access to the U.S. Market

Through its Skelmersdale lab, Element’s new NRTL designation removes the need for multi-site testing and U.S. hand-offs, accelerating time-to-market for manufacturers targeting the U.S.

Element, one of the world’s leading providers of laboratory-based testing, inspection and certification services, today announced a major milestone in its global certification capability. Its Skelmersdale, UK, laboratory has been officially recognised by the United States government as a Nationally Recognized Testing Laboratory (NRTL) for Hazardous Locations. This recognition, a first for the UK, authorises Element Skelmersdale to conduct testing and issue NRTL certification for manufacturers seeking access to the U.S. market.

Representing a significant step forward for Element and its customers worldwide, this latest achievement strengthens the company’s ability to support manufacturers of equipment used in explosive and hazardous environments with faster, more streamlined access to critical U.S. certifications.

With this designation, Element Skelmersdale becomes the first and only UK‑based NRTL authorised to issue U.S. certification for hazardous locations directly from within the UK. It is also the first and only UK‑based NRTL able to carry out evaluation, testing, and certification for hazardous locations in a single location, removing the multi‑site process that is typically required across the industry. As a result, manufacturers benefit from a dramatically simplified certification pathway and accelerated routes to market for hazardous‑location products.

Element’s new NRTL status delivers clear and tangible benefits for customers. The laboratory now has full control of the certification process, enabling Element to issue NRTL certification independently without reliance on third‑party certification bodies in the United States. Certification can be issued directly from the UK, significantly reducing turnaround times by eliminating the need to transfer reports overseas for final approval. Greater efficiency and reduced dependency on external laboratories also support improved cost management for manufacturers.

Commenting on the achievement, Fabian Schober, SVP of Element’s Connected Technology & Mobility (CT&M) business unit, said: “Achievements like this underline our long‑term commitment to investing in capabilities that deliver real value for our customers. This recognition reflects the dedication, expertise, and collaboration of teams across our business and within our Skelmersdale laboratory.  I want to sincerely thank everyone who contributed.”

Further details on the designation are available via the official announcement in the U.S. Federal Register here.